Full Specifications
| Item number | Diameter | Segment width | Segment height | Arbor |
|---|---|---|---|---|
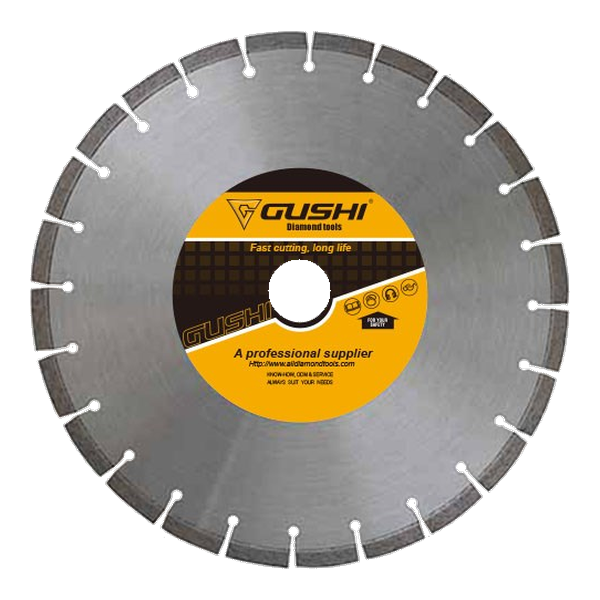
| 12HCSB | 12 in / 300 mm | 3.0 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 14HCSB | 14 in / 350 mm | 3.2 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 16HCSB | 16 in / 400 mm | 3.6 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 18HCSB | 18 in / 450 mm | 3.8 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 20HCSB | 20 in / 500 mm | 4.0 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 24HCSB | 24 in / 600 mm | 4.5 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 28HCSB | 28 in / 700 mm | 4.5 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 30HCSB | 30 in / 750 mm | 4.5 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 32HCSB | 32 in / 800 mm | 4.5 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 36HCSB | 36 in / 900 mm | 4.5 – 6.0 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 40HCSB | 40 in / 1000 mm | 5.5 – 6.5 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 44HCSB | 44 in / 1100 mm | 5.5 – 6.5 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| 48HCSB | 48 in / 1200 mm | 5.5 – 7.0 mm | 10 / 12 mm | 22.23 / 25.4 mm |
| Rim | A-segmented |
|---|---|
| Joint | Laser welded segment to core |
| Materials | Block, brick, concrete, masonry, stone |
| Industries | Construction, industrial, masonry and stone, MRO, rental |
| Machines | Gas powered saw, stationary saw, flat saw, walk behind saw |
| Other sizes | More specifications and styles available on request |
Why These Blades Are Welded, Not Brazed
There are three ways to hold a diamond segment on a steel core, and the difference between them decides how large a blade can safely be. The oldest is a sintered or hot pressed segment bonded to the blank. The next is brazing, where a filler alloy sits between segment and core. The third is a laser weld, which melts a narrow zone of segment and core together so the joint is the same metal as the parts it joins.
A braze is strong enough for a hand held blade, and it is the reason the small sizes in the market are cheap. What it does not like is heat and tangential load together. The load at the rim of a circular blade rises with diameter, because the same cut is being made further from the centre, and the joint on a 1200 mm blade is asked to hold a segment that is travelling a four times longer path than the one on a 300 mm blade. A filler alloy is a layer of a third metal sitting in that load path. A weld has no third metal.
The second thing welding buys is thermal. A brazed joint can be softened by the heat of a dry cut, and once the filler has been softened the segment can shift or lift. A weld has no filler to soften, which matters on a gas powered saw where the operator may be cutting dry with no water on the joint.
The trade is honest and it should be stated. A welded segment cannot be replaced the way a brazed one can, and once the segment is worn to the weld line the blade is finished: the core cannot be re-tipped without a new weld, and a core that has been scored in the cut is not a safe carrier for a new segment. A welded blade is bought to be used up, not to be rebuilt, and it is priced and specified on that basis.
The Width Ladder from 300 to 1200 mm
Segment width is not constant across this range, and the way it climbs tells you what the large sizes are actually doing. The blade starts at 3.0 mm at 300 mm and reaches 5.5 to 7.0 mm at 1200 mm, roughly doubling over a fourfold increase in diameter.
Two things drive it. The first is the depth of the slot. A 300 mm blade cuts about 150 mm deep and a 1200 mm blade about 600 mm, and the deeper the slot the more slurry has to travel back out of it past the core. A narrow kerf on a deep cut packs the slot, the slurry recirculates around the segment and the blade stops cutting while the segment is still sharp. Widening the segment gives that slurry somewhere to go.
The second is stiffness. The core of a large blade is a thin disc reaching a long way from the flange, and the side load on it during a cut is carried by the tension in the core rather than by its thickness. A blade that flexes at the rim cuts a slot that wanders, and a wandering slot in a deep cut pinches the blade and loads the segment on one side only. The extra width at the rim is part of keeping the cut straight.
Rim Speed and Why the Big Ones Turn Slow
The single most useful piece of arithmetic on this page is this: rim speed is circumference multiplied by spindle speed, so at the same spindle speed a blade of twice the diameter runs at twice the rim speed. Nothing about the segment changes; the same diamond is simply meeting the concrete twice as fast.
That is why a 1200 mm blade does not sit on the arbor of a saw built for a 300 mm blade, and why the large sizes in this range belong on flat saws and walk behind saws with their own gearing. The machine is not stronger because the blade is bigger. The machine is built to turn a big blade at a lower spindle speed so that the rim speed at the segment stays inside the range the bond was designed for.
Run a segment too fast and three things follow in order. The bond wears before the diamond has done its work, so the segment glazes and stops cutting. The heat at the segment rises quicker than the water can carry it away. And the weld and the core are asked to carry a load they were not specified for. All three show up as a blade that seems to have stopped working long before it has worn out.
Ten or Twelve Millimetres of Segment
Every size in this range carries a segment 10 or 12 mm high, from the 300 mm blade to the 1200 mm one. That consistency is easy to read past, and it is the most commercially important number in the table.
The segment height is the wear reserve, the depth of diamond available before the blade is finished. Because it does not grow with diameter, the amount of diamond on the rim grows only with the number of segments, while the length of rim grows with the diameter. A 1200 mm blade has a rim about four times as long as a 300 mm blade. If both carry the same 12 mm of segment, then the cost of diamond per metre of cut is far higher on the big blade, and the only thing that justifies it is that the big blade is doing work the small one cannot reach at all.
This is why the choice of diameter is a cost decision before it is a specification decision. If a 450 mm blade will reach the depth the job needs, buying a 600 mm blade does not buy a longer-lived blade. It buys more diamond, more core, a heavier saw and a wider kerf, on a blade that has to be worn down over the same 10 or 12 mm as the smaller one.
Water, Slurry and the Flat Saw
On a flat saw, water is not a comfort feature. It is part of the cutting system, and a large diamond blade run without it is being asked to do the work with two of its three functions removed.
The first function is dust. Cutting concrete, block and stone raises silica dust at the cut, and water suppresses it where it is made rather than downstream of the operator’s lungs. The second is cooling: the segment is doing work against a hard, abrasive material, and the heat has to leave somewhere. The third, and the one people forget, is flushing. A deep cut in a large blade produces a volume of slurry, and if it is not carried out of the slot it packs around the segment, blinds the diamond and turns the cut into a rub.
That is the physical reason the segment widens as the diameter grows. A wider slot is a slurry channel. On the large sizes, water volume matters more than water pressure: a steady flow that keeps the slot wet and moving is worth more than a high pressure jet that wets one spot. Check the flow at the blade before the first cut, not at the pump.
Matching Blade to Saw
The range is built around four machine types, and the blade should be chosen from the machine backwards rather than from the depth forwards. Get that order right and most of the specification questions answer themselves.
Gas powered saws
These run the small and middle diameters, typically 300 to 400 mm, and they are the machines most often used dry. They are also the machines where the laser welded joint earns its place, because a dry cut puts heat into the segment and the joint with nothing to carry it away.
Stationary and masonry saws
Bench saws with a water tray run 350 to 500 mm and cut block, brick and pavers all day. The blade is supported by the table rather than by the operator’s hands, so the cut is straight and the segment is loaded evenly. This is the easiest life a diamond blade has.
Flat saws and walk behind saws
These carry the large diameters, from about 450 mm up to 1200 mm, and they are the reason the top of the range exists. The blade is heavy, the machine is heavy, and the cut is usually in a slab, a road, a runway or a wall. Everything about the setup matters more here: flange condition, arbor fit, water flow and the alignment of the guard.
Whichever machine, the rule is the same. The blade diameter must be inside the machine’s marked capacity, the guard must cover the arc the machine was designed to cover, and the arbor bore must be the machine’s bore rather than an adapter that nearly fits. On a large blade a loose fit is not a vibration problem, it is a blade that can climb.
Concrete, Block, Brick, Masonry, Stone
Five material families are listed for this blade, and they are not five versions of the same job. What changes between them is how the material fails under the segment, and that decides the feed, the water and the depth of each pass.
Concrete is a composite of aggregate in a cement matrix, and the segment meets hard stones and soft matrix in the same centimetre. It rewards a steady feed and generous water, and it punishes a heavy hand by glazing the bond. Cured concrete is abrasive as well as hard, so a concrete blade wears visibly in normal use; that wear is the blade working, not the blade failing.
Block and brick are softer and more brittle. They cut easily and they break easily, so the risk is not the blade but the workpiece: a block that spalls ahead of the cut gives a ragged edge and can pinch the blade. Shallow passes and a supported workpiece solve both. On brick, expect the mortar joints to cut differently from the brick itself, and do not read a change in the sound as a fault.
Masonry as a category covers everything from soft limestone to hard granite in a wall, and stone is the family where the segment’s bond matters most. Hard, dense stone wears a soft bond quickly and keeps the diamond exposed, which is what you want; a hard bond on the same stone polishes and stops cutting. If a blade that worked on concrete stops cutting on granite, the answer is a different bond rather than more pressure. The same logic runs through the rest of the continuous rim and segmented range, where the material decides the rim before the diameter does.
Reinforced Concrete and What It Does to a Rim
Reinforced concrete is where a concrete blade meets steel, and the meeting is uncomfortable. The segment is designed to grind a brittle, abrasive material; rebar is ductile and it cuts by a different mechanism. A segment that is spending part of each revolution in steel behaves differently from one that is spending all of it in concrete.
The usual symptom is a blade that goes through the concrete and then stops cutting at the depth where the steel sits. The bond has glazed on the steel, the diamond is no longer standing proud, and more pressure makes it worse rather than better. The correction is to dress the rim on abrasive material, restore the water, and come back with a lighter feed so the segment keeps cutting rather than rubbing.
Knowing where the steel is before the first cut is worth more than any technique afterwards. A cover meter, a drawing or a trial cut in a hidden corner will tell you the depth of the first mat, and that lets the operator expect the change in sound and the change in feed rather than discover it. On a wall or a slab being cut for a door or a penetration, the steel is usually where the structural engineer put it, which is usually where the cut needs to go.
For work that is more steel than concrete, or for reinforced sections that will be cut repeatedly, the tool changes rather than the blade. A sintered diamond wire saw takes reinforced sections at depth without a circular blade’s reach limit, and core drilling takes the hole rather than the slot, using concrete core drill bits and their diamond segments.
Depth of Cut and Step Cutting
The depth ceiling for any circular blade is its radius, less whatever the flange, the hub and the machine’s own geometry take out of it. That gives about 150 mm at 300 mm, about 300 mm at 600 mm and about 600 mm at 1200 mm as the arithmetic limit, and rather less in practice on a flat saw.
Where a job needs more depth than one pass gives, the answer is steps rather than force. A first pass at a shallow depth establishes the line and lets the operator see what the material is doing; the second pass follows the same line deeper. Cutting in steps is slower per pass and quicker per job, because a blade that is loaded to its limit in one pass wanders, glazes and gets pinched, and the recovery costs more than the extra pass would have.
Step cutting also protects the machine. A flat saw asked to take its maximum depth in one pass loads the engine, the belt and the blade at the same moment, and the reaction when the blade grabs is taken by the operator’s arms. On the large diameters, two or three passes at increasing depth are the normal way to work, and the blade lasts longer for it.
One more thing belongs here. A cut that is deeper than the blade’s radius cannot be made by any circular blade, whatever the diameter, and no amount of stepping changes that. When the depth required exceeds the radius, the tool is wrong and the answer is a wire saw or a different method, not a bigger blade. The split turbo blade covers the hand held masonry work that sits below this range, and the brazed concrete blade covers the smaller diameters where a welded joint is not necessary.
Reading Wear and Retiring a Blade
A diamond blade tells you what is happening to it, and the reading is taken at the rim rather than at the arbor. Three patterns cover most of what an operator needs to know.
The first is even wear across the segment, with the diamond standing proud and the segment face grey and gritty. That is the blade working correctly. Keep the water and the feed where they are. The second is a shiny, polished segment face with the diamond no longer visible, which is glazing: the bond has worn away quicker than the diamond was consumed, or the blade has been run hot or too fast. It is corrected by dressing, not by pressure. The third is uneven wear, with one side of the segment lower than the other, which points at a blade running out of alignment: a bent flange, a worn arbor, or an operator leaning the saw.
The retirement point on a laser welded blade is the weld line. When the segment is worn down to where the weld meets the core, the blade is finished. Continuing past that point puts steel into the cut, which is not cutting, and it scores the core at exactly the place that has to carry the next load. A worn core is not a candidate for re-tipping; it is scrap, and it should be treated as scrap rather than kept in the van as a spare.
Private Label and Export Supply
The range is made to order as well as stocked, and the specification is fixed per diameter before the run starts. That matters because the sizes are not simply scaled: width, core thickness and the segment bond all change along the ladder, so a private label order is placed as a set of sizes rather than as one blade in thirteen lengths.
What can be set for a private label order: the diameter list, segment width and height for each size, the arbor bore, the core printing on both faces, and the sleeve or carton print. Where a distributor sells into more than one market, splitting 22.23 mm and 25.4 mm across one order is normal, since those two bores cover most flat saws and walk behind saws in service.
For the rest of the cutting range, the dry cutting segmented blade and the hot pressed segmented blade cover general masonry work in the smaller diameters, the asphalt and concrete blade covers green concrete and asphalt where this bond would glaze, the hand held saw blade covers the small machines, and the carbide grit cup wheels cover the grinding rather than cutting side of the same jobs.
Frequently Asked Questions
- What is a laser welded diamond blade?
- A diamond blade whose segments are joined to the steel core by a laser weld rather than by brazing or by sintering the segment onto the blank. The weld fuses segment and core into one piece of metal, so the joint does not depend on a filler alloy. That is what makes it practical to build the same blade from 300 mm up to 1200 mm for walk behind saws.
- What sizes are available?
- Thirteen diameters: 300, 350, 400, 450, 500, 600, 700, 750, 800, 900, 1000, 1100 and 1200 mm, which is 12, 14, 16, 18, 20, 24, 28, 30, 32, 36, 40, 44 and 48 inch. All take a 22.23 mm or 25.4 mm arbor, and all use a segment 10 or 12 mm high.
- Why does segment width change with diameter?
- Because depth of cut changes with diameter. A 300 mm blade cuts about 150 mm deep and a 1200 mm blade about 600 mm, so the bigger blade has to clear far more slurry out of a much deeper slot and has to stay rigid over a longer reach into the cut. The width steps from 3.0 mm at 300 mm to 5.5 to 7.0 mm at 1200 mm to carry that load.
- Which saw runs which diameter?
- Hand held and small gas powered saws run the 300 and 350 mm blades. Stationary saws and masonry bench saws take 350 to 500 mm. Flat saws and walk behind saws take the large diameters, from about 450 mm up to 1200 mm, and those are the machines the top of the range is built for. Match the blade to the machine’s marked capacity and guard.
- Does a bigger blade mean a quicker cut?
- It cuts deeper, not necessarily quicker. Rim speed is what does the cutting, and rim speed is diameter multiplied by spindle speed, so a blade of twice the diameter runs at twice the rim speed if the spindle speed is unchanged. Large blades are therefore run on machines geared for them. Forcing a big blade at a small blade’s spindle speed overloads the segment and the saw.
- What materials is it for?
- Concrete, block, brick, masonry and stone, on construction, industrial, masonry and stone, MRO and rental work. It is a concrete saw blade first. Asphalt is a different bond and a different segment, and metal cutting wants a blade built for metal rather than a concrete blade pushed into steel.
- Dry or wet cutting?
- The listing does not state a dry or wet rating, and the answer follows the machine rather than the blade. Flat saws and walk behind saws are normally run with water for dust control and to flush slurry out of the cut. Gas powered saws on site are often run dry. Ask for the rating for the specific size you are ordering.
- What does 10 or 12 mm segment height mean in practice?
- It is the wear reserve, and it is the same on a 300 mm blade and a 1200 mm blade. That is worth noticing: a 1200 mm blade carries a rim about four times as long as a 300 mm blade with the same 10 or 12 mm of diamond on it, so the cost of the diamond per metre of cut rises sharply with diameter. Buy the smallest diameter the job allows.
- Can it cut reinforced concrete?
- It will cut through reinforcement, and the steel is what governs the segment. A concrete segment that meets rebar has to grind steel as well as stone, which glazes a hard bond and rounds a soft one. Expect to dress the rim on abrasive material if the blade stops cutting after a run of reinforced work, and find out where the steel is before the first cut.
- How deep will each size cut?
- The ceiling is the radius less whatever the flange and the machine take, so a 300 mm blade reaches about 150 mm, a 600 mm about 300 mm and a 1200 mm about 600 mm. In practice a flat saw cuts less than the radius because the arbor and guard sit in the way, and deep work is done in steps rather than in one pass.
- When should the blade be retired?
- When the segment is worn down to the weld line and the steel core starts to show at the rim. A laser welded blade cannot be re-tipped the way a brazed blade can, and a core that has been touched by the cut is no longer a safe carrier for a new segment. Retire it at the weld line, not after the core has been scored.
- Can you supply these under our brand?
- Yes. Diameter, segment width and height, arbor bore, core printing and packaging are made to order, and the diameter range means a distributor can cover hand held work and flat saw work from one supplier. Send the saw models, the diameters you sell and the material mix in your market.