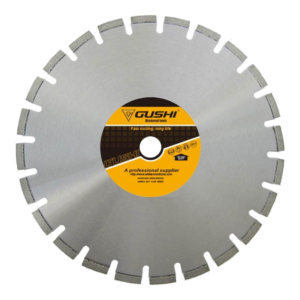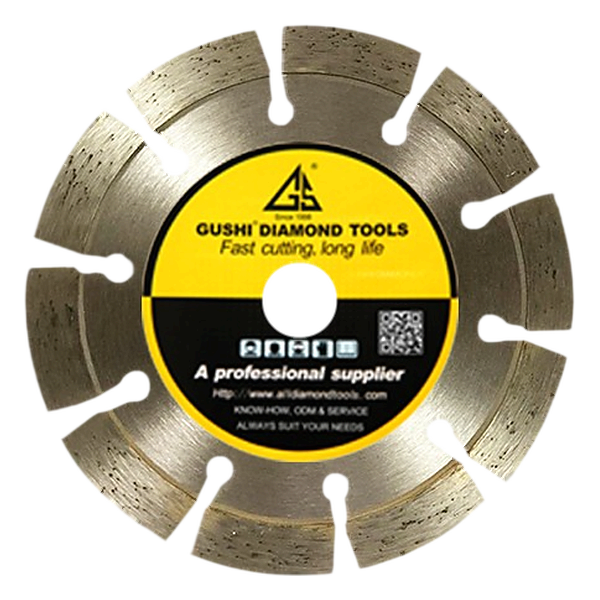
Full Specifications
| Parameter | Specification |
|---|---|
| Product type | Hot pressed segmented diamond cutting blade, open gullet rim |
| Process | Hot pressed sintered segment on alloy steel core, pressure applied during sintering |
| Diameter range | 110 mm to 350 mm, 8 sizes |
| Segment height | 10 mm on every size |
| Segment width (kerf) | 1.8 mm at 110 and 125 mm; 2.0 mm at 150 mm; 2.2 mm at 180 mm; 2.3 mm at 230 mm; 2.5 mm at 250 mm; 2.8 mm at 300 mm; 3.0 mm at 350 mm |
| Segment number | 10, 10, 12, 12, 15, 17, 21 and 23 from 110 to 350 mm |
| Arbor bore | 20 mm at 110 and 125 mm; 22.23 mm at 150 to 250 mm; 25.4 mm at 300 and 350 mm |
| Bond | Hard to medium hard matrix for abrasive masonry and concrete |
| Cutting mode | Wet or dry; water recommended wherever it is available |
| Rim speed reference | 80 m per second class; see the speed table below |
| Core | Tensioned alloy steel core with laser cut keyhole gullets |
| Standard | Conforms to EN13236; manufactured under ISO 9001; CE marked |
| Tested life, granite slab | 200 m on 16 mm granite in factory bench test, wet |
| Tested life, hard granite | 120 m on Indian black granite in factory bench test, wet |
| Monthly capacity | More than 200,000 pieces, batch cutting tested with retained sample |
| Quality system | AQL 2.5 inspection, in-process testing, batch number traceable to retained sample |
How the Segmented Rim Cuts
The diamond is not sharp
Diamond in a segment works by scratching, not by slicing. Each crystal removes a few microns per pass, and once the crystals at the surface blunt or are pulled out, the metal matrix around them has to wear back to expose the next layer. That balance is the bond. A matrix that is too hard holds blunt diamond and the segment polishes; one that is too soft lets the diamond fall out before it has done any work. Concrete and brick are abrasive, so this blade runs a hard to medium hard bond, which is the opposite of what granite needs.
Why the gullets are wide and open
The gaps between segments are the cooling and clearing system. Every revolution, each gullet carries dust and slurry out of the cut and pulls air or water in behind it. On concrete that dust load is heavy, and a rim without open gullets packs solid within a metre or two of cutting, which is when the blade stops cutting and starts rubbing. The cost of a wide gullet is an interrupted cut: on polished stone the exit edge chips where each segment leaves the material. That is why this rim belongs on structural and masonry work, and a closed rim belongs on finished stone.
What hot pressing adds
In hot pressing, the segment is sintered while the mould is still under mechanical pressure, so the metal matrix reaches a higher density than a cold pressed segment that is shaped first and fired afterwards. A denser matrix grips each diamond harder and resists the impact loading that breaks segments on site. The practical benefit is not a sharper blade but a more predictable one: the segment keeps its shape, the cutting rate stays flat across its life, and the blade survives being dropped, pinched or run out of alignment, which is how most blades actually die.
Key Features Explained
10 mm segment height on every diameter
Ten millimetres of diamond depth is a deliberate commercial choice, not a spec sheet accident. It gives enough reserve to finish a footing, a slab edge or a wall opening without a blade change, and a blade change in the middle of a job costs more than the difference between a 7 mm and a 10 mm segment. It also keeps one segment specification across the whole range, which matters to a distributor carrying eight sizes.
Segment count scaled to diameter
The number of segments rises from 10 at 110 mm to 23 at 350 mm, so the length of each individual block stays roughly comparable as the circumference grows. More, shorter segments means more gullet length per revolution, which is how the large diameters keep coolant reaching the rim at 80 metres per second. A 350 mm blade built with 12 long segments instead would run hotter and load up faster.
One range from trim work to floor saws
The 110 mm and 125 mm sizes with a 20 mm bore cover small grinders and the 20 mm spindles common on European and Asian tile saws. The 150 to 230 mm sizes with 22.23 mm bore are the angle grinder and masonry saw sizes. The 250 mm size bridges to small floor saws, and 300 and 350 mm with a 25.4 mm bore are floor saw and bridge saw sizes. An eight size range means a distributor can supply a full site from one supplier and one bond specification.
Tested, not estimated, life figures
Two factory bench tests define what this blade does in stone. On a 16 mm granite slab, wet, it cut 200 metres before the segment was consumed. On Indian black granite, one of the hardest and most abrasive commercial granites, the same specification reached 120 metres. Concrete and block are far more abrasive than either, so site life there is shorter and is governed more by rebar content and machine power than by the blade.
Batch traceability for repeat orders
Every production batch is cutting tested and a bulk sample is retained under the batch number. For a distributor this is the difference between buying a blade and buying a specification: if a container performs differently from the last one, the batch number leads back to the retained sample and the test record. It is also what makes OEM supply with a stable bond possible across repeat orders.
Selection Guide
Match the diameter to the machine first, then read the segment count and kerf off the same row. All eight rows share the same 10 mm segment height.
| Diameter | Arbor bore | Segment width | Segments | Typical machine | Arithmetic max rpm at 80 m/s |
|---|---|---|---|---|---|
| 110 mm | 20 mm | 1.8 mm | 10 | 100 mm angle grinder | 13,890 |
| 125 mm | 20 mm | 1.8 mm | 10 | 125 mm angle grinder | 12,220 |
| 150 mm | 22.23 mm | 2.0 mm | 12 | Angle grinder, tile saw | 10,190 |
| 180 mm | 22.23 mm | 2.2 mm | 12 | 180 mm angle grinder, masonry saw | 8,490 |
| 230 mm | 22.23 mm | 2.3 mm | 15 | 230 mm angle grinder, masonry saw | 6,640 |
| 250 mm | 22.23 mm | 2.5 mm | 17 | Masonry saw, small floor saw | 6,110 |
| 300 mm | 25.4 mm | 2.8 mm | 21 | Floor saw, bridge saw | 5,090 |
| 350 mm | 25.4 mm | 3.0 mm | 23 | Floor saw, bridge saw | 4,370 |
The rpm column is arithmetic from the 80 metre per second rim speed class, not a factory recommendation. The marking on the blade and the rating plate on the machine govern, and the lower figure always applies.
Applications and Materials
| Application | Fit | Note |
|---|---|---|
| Plain and reinforced concrete | Best | Pass rebar at reduced feed; expect faster segment wear at steel |
| Brick and block walls | Best | Dry cutting acceptable for short passes with idle cooling |
| Pavers and kerbs | Best | Use water on site to control silica dust |
| Roof tile and slate | Good | Small diameters, low feed, expect a chipped exit edge |
| Sandstone and limestone | Good | Abrasive stone, high wear, steady feed keeps the cut straight |
| Granite and hard stone, rough work | Good | 200 m on 16 mm granite; use a turbo rim where the edge is visible |
| Asphalt | Acceptable | Works, but a dedicated asphalt blade with a different bond lasts longer |
| Polished slab for a visible edge | Not ideal | Open gullets chip the exit edge; use a turbo or continuous rim |
| Material | Abrasiveness | Wet or dry | Behaviour with this blade |
|---|---|---|---|
| Concrete, cured | High | Wet | Steady cut, bond wears evenly, rebar is the limit |
| Brick, clay | High | Dry or wet | Very fast, low load, longest relative life |
| Concrete block | Medium | Dry | Fast, gullets stay open, good for dry site work |
| Sandstone | Very high | Wet | High wear, keep feed light and water on the segment |
| Granite | Medium | Wet | 120 to 200 m in bench tests, slower than in concrete |
| Marble | Low | Wet | Cuts easily but chips at the exit edge; use a closed rim for finish |
How to Use It
- Check the bore before mounting. 110 and 125 mm blades have a 20 mm bore, 150 to 250 mm have 22.23 mm, and 300 and 350 mm have 25.4 mm. A loose blade on the wrong spindle will crack at the flange.
- Match the flange. The clamping flange should be at least one third of the blade diameter. An undersized flange is the most common cause of a wandering cut.
- Confirm the direction arrow. The arrow on the blade points in the direction of rotation. Running backwards polishes the segment and the blade will not cut.
- Check the machine speed. Compare the blade marking with the machine rating plate and run the lower of the two. This matters most on 300 and 350 mm blades on high speed saws.
- Set water if you have it. Aim the flow at the segment entering the cut and check the rate, not just that water is present. Dry cutting is for short passes only.
- Start the cut with the blade clear. Let the blade reach full speed before contact, then enter the material at a steady feed. Slamming into the edge is what breaks segment roots.
- Keep the feed steady. Too light a feed glazes the segment; too heavy a feed overloads the spindle and can stall the blade. A steady rate with visible dust or slurry leaving the gullets is correct.
- Do not lever the blade. Side pressure in a deep cut bends the core and pinches the blade. If the cut closes behind the blade, wedge it open.
- Run dry passes in cycles. Cut for 20 to 30 seconds, then idle the blade in air for the same time so the core can shed heat. Continuous dry cutting warps the core and softens the braze.
- Dress the rim when it stops cutting. A few passes in abrasive block, sandstone or a dressing brick restores the cutting action. If it glazes again within a metre, the bond is wrong for the material, not the blade.
- Retire it at the marker. Stop using the blade when the segment reaches the wear line or the segment height approaches 2 mm. A worn blade on a high speed saw is a burst risk, not a slow blade.
Frequently Asked Questions
- What is a hot pressed segmented blade and what is it used for?
- It is a diamond blade whose rim is cut into separate segments with wide open gullets between them, and whose segment is sintered under mechanical pressure rather than pressed cold and fired. The open gullets throw slurry and heat out of the cut, which suits abrasive, dirty work: concrete, reinforced concrete, brick, block, pavers, roof tile, slate and rough stone. It is the general purpose blade on most sites.
- Hot pressed or cold pressed, what is the real difference?
- In hot pressing the mould is held under pressure while the metal bond sinters, so the matrix reaches a higher density and grips each diamond more tightly. A cold pressed segment is shaped first and sintered afterwards without that pressure. The practical result is a segment that resists breakage, holds its shape longer and cuts at a steadier rate across the life of the blade, at a higher unit cost than cold pressed.
- How long will this blade last in granite?
- Our factory test on a 16 mm granite slab reached 200 metres of cut. On Indian black granite, which is one of the hardest and most abrasive commercial granites, the same blade reached 120 metres. Both figures are from controlled bench tests with water, and real site life depends on machine power, feed pressure and how much steel rebar is in the cut.
- Which diameters are available and which machines do they fit?
- Eight diameters: 110, 125, 150, 180, 230, 250, 300 and 350 mm. The 110 to 150 mm sizes run on 100 and 125 mm angle grinders and small tile saws, 180 and 230 mm on large angle grinders and masonry saws, 250 mm on masonry and small floor saws, and 300 and 350 mm on floor saws and bridge saws. Bore is 20 mm on 110 and 125 mm, 22.23 mm on 150 to 250 mm, and 25.4 mm on 300 and 350 mm.
- Why does this blade only come in 10 mm segment height?
- Ten millimetres is the standard reserve for general purpose site work: it gives enough diamond depth to finish a slab, a footing or a wall opening without a blade change, which is where the money is lost. Thinner 7 mm segments exist for grinders used on trim work, and they are cheaper, but on a 230 mm and above blade the segment cost is a small share of the total and running out mid job is expensive.
- Can it cut reinforced concrete?
- Yes, with care. A hot pressed segmented blade cuts reinforced concrete and will pass through rebar, but diamond is not the right abrasive for steel and the segment wears fast at the steel. Expect noticeably shorter life in reinforced sections than in plain concrete, reduce feed pressure over the bar, and use water. For daily rebar cutting, a laser welded blade with a tougher bond is the better tool.
- Should I cut wet or dry?
- The blade is rated for both. Wet cutting is always better where water is available: it removes heat from the segment, keeps the gullets from packing with dust and suppresses respirable crystalline silica, which is a regulated health hazard in most markets. Dry cutting is acceptable for short passes in brick, block and tile, and for that work run 20 to 30 second cuts with an equal idle period between them.
- Why does my segmented blade wander or cut slowly?
- Three usual causes. A worn or undersized flange lets the blade flex, so check the flange diameter is at least a third of the blade diameter. Gullets packed with dust stop clearing, so dress the rim in abrasive block or concrete. And a glazed rim, where the segment looks shiny and polished, means the bond is too hard for the material; open it in sandstone or a dressing brick, then increase feed pressure.
- What is the difference between this blade and a turbo rim blade?
- The segmented blade has wide open gullets and clears slurry fastest, which makes it the efficient choice for concrete, brick and block where the cut edge is hidden. A turbo rim keeps the band continuous with narrow slits, which cuts granite and quartz faster and leaves a much smaller chip on a visible edge. Use the segmented blade for structure and masonry, the turbo rim for finished stone.
- How do I read the segment number on the size table?
- Segment number is how many separate diamond blocks sit on the rim, and it falls as diameter grows: 10 segments at 110 and 125 mm, 12 at 150 and 180 mm, 15 at 230 mm, 17 at 250 mm, 21 at 300 mm and 23 at 350 mm. More segments means shorter individual blocks and more gullet length per revolution, which improves cooling at high rim speed on the large diameters.
- What is the maximum safe speed for each diameter?
- This blade class is built to an 80 metre per second rim speed. The arithmetic maximum at that speed is about 13,890 rpm at 110 mm, 12,220 at 125 mm, 10,190 at 150 mm, 8,490 at 180 mm, 6,640 at 230 mm, 6,110 at 250 mm, 5,090 at 300 mm and 4,370 at 350 mm. These are calculated figures, not factory markings: the marking on the blade and the rating plate on the machine govern, and the lower of the two is the limit.
- What is the MOQ, the lead time and can I get my own brand?
- Standard MOQ is 50 pieces per size, and mixed diameter orders are accepted. Lead time is 25 to 30 days from order confirmation, shorter for stock sizes. OEM covers laser marking, printed flange labels, colour boxes and bespoke diameter, segment height, segment count, bond hardness and arbor. Monthly capacity is above 200,000 pieces, and every production batch is cutting tested with a retained sample kept for comparison.