Full Specifications
| Item | HSSGT series turbo rim diamond blade with protect teeth |
|---|---|
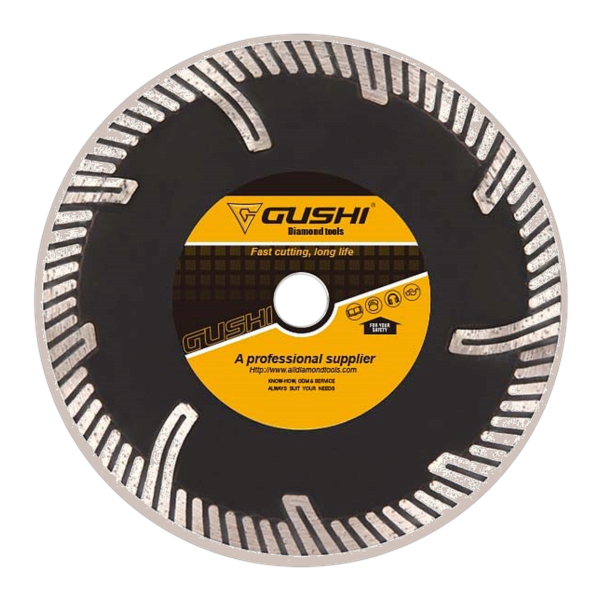
| Construction | Continuous turbo rim, laser welded to a steel core with side protect teeth |
| Diameters | 100, 115, 125, 150, 180, 200, 230, 250, 300 and 350 mm |
| Segment width (kerf) | 2.0 mm at 100 mm, rising to 3.2 mm at 350 mm |
| Segment height | 8 mm as standard; other heights arranged to order |
| Arbor | 16, 20, 22.23 or 25.4 mm; reducing bushings to order |
| Rim type | Continuous band with a waved turbo edge and side protect teeth |
| Cutting mode | Wet or dry |
| Materials | Granite, marble, hard stone, masonry, brick, tile |
| Machine types | Angle grinder, tile saw, hand-held stone saw, small bench saw |
| Packing | Individual sleeve, then export carton; 25 to 50 pcs per carton by size |
| Standards | Made under ISO 9001; finished blades carry the CE mark |
What the Protect Teeth Actually Do
A standard rim blade only cuts on its face. The side faces of the rim sit flush with the steel core, so in a plunge cut or a deep slot the wall of the cut is finished by the core plate rubbing against the stone. That rubbing heats the core, dishes it, and leaves the slot wall ragged. The protect teeth break that pattern.
Side teeth that true the wall
The protect teeth are short diamond segments welded proud of the core on both sides of the rim. They reach the wall of the cut before the core does, so they dress the wall square as the blade goes down. The slot comes out clean on both faces instead of nibbled, and the core plate never touches the stone on its sides. The teeth also carry side load: without side support the core flexes and the cut closes on the rim, so the protect teeth hold the disc on diamond rather than on bare steel.
Protecting the core from heat
A core that rubs on the sides heats locally, and steel that heats loses tension and dishes. A dished core binds in the cut, which adds more heat, and the spiral ends with a blade that will not run true. The protect teeth keep the core clear of the stone, so the disc stays flat through a long dry run that would dish a plain rim.
A stock feature, not an option
The protect teeth are part of the standard HSSGT build, not a paid extra. Every diameter leaves the works with the side teeth in place, so a distributor gets the same profile across the range and a re-order behaves like the first.
What a Continuous Turbo Rim Does
The rim is a single band of diamond bond with a wave pressed into its outer edge. It is continuous around the whole circumference, so the diamond is in the cut the entire way round.
Constant contact, smooth cut
Because the band never breaks, the rim strikes the stone once and stays there. A segmented blade leaves and re-enters the cut at every gullet, which is what leaves the scalloped exit edge on a granite slab. A continuous rim tracks straight and the edge comes away clean. The trade for that smoothness is that a flat continuous rim polishes itself shut after a few metres, because there is nowhere for the slurry to go. The turbo wave in the edge solves that.
The wave gives the rim shallow channels that carry water in and swarf out, leaving the bond edges exposed so the metal wears back and fresh diamond comes up. Because the wave is shallow, the rim still meets the stone as an almost continuous edge.
Why constant contact matters for chip-free work
A chip at the exit edge is almost always the rim leaving the stone and re-biting it. With the rim in contact the whole way round, the stone is supported right up to the break point, so the edge lifts away instead of tearing. The protect teeth add the side support the face alone cannot give.
The wave is not a gullet
People see the waved edge and read it as a segmented blade with narrow slots. It is not. There is no break in the rim anywhere on the circumference; the wave is a form pressed into the band, not a cut through it. That is the point: a continuous rim for a smooth cut, with the wave doing the clearing that gullets would otherwise do.
Size Chart: Diameter, Segment Width, Arbor and Speed
| Item | Diameter | Segment width | Segment height | Arbor | Max rpm |
|---|---|---|---|---|---|
| 4HSSGT | 4 in / 100 mm | 2.0 mm | 8 mm | 16 / 20 / 22.23 mm | 15,300 |
| 4.5HSSGT | 4.5 in / 115 mm | 2.0 mm | 8 mm | 16 / 20 / 22.23 mm | 13,300 |
| 5HSSGT | 5 in / 125 mm | 2.2 mm | 8 mm | 20 / 22.23 mm | 12,200 |
| 6HSSGT | 6 in / 150 mm | 2.4 mm | 8 mm | 20 / 22.23 mm | 10,200 |
| 7HSSGT | 7 in / 180 mm | 2.4 mm | 8 mm | 22.23 / 25.4 mm | 8,500 |
| 8HSSGT | 8 in / 200 mm | 2.6 mm | 8 mm | 22.23 / 25.4 mm | 7,600 |
| 9HSSGT | 9 in / 230 mm | 2.6 mm | 8 mm | 22.23 / 25.4 mm | 6,600 |
| 10HSSGT | 10 in / 250 mm | 2.8 mm | 8 mm | 22.23 / 25.4 mm | 6,100 |
| 12HSSGT | 12 in / 300 mm | 3.0 mm | 8 mm | 22.23 / 25.4 mm | 5,100 |
| 14HSSGT | 14 in / 350 mm | 3.2 mm | 8 mm | 22.23 / 25.4 mm | 4,400 |
Segment width widens with diameter because a larger disc needs a stiffer rim to hold its line, and above 250 mm the blade is usually on a saw. Segment height is 8 mm across the range as standard; other heights are arranged to order.
Choosing a Segment Height
The diamond lives in the segment and nowhere else. Once the segment is down to about 1.5 mm above the steel, the blade is cutting stone with a steel edge: it stops cutting, it heats up, and it can crack at the weld. Segment height is the working life of the blade, and the standard 8 mm height here is aimed at mixed stonework rather than a single light duty.
| Segment height | Usable band | What it suits |
|---|---|---|
| 8 mm (standard) | about 6.5 mm | Mixed granite, hard stone, masonry and brick where one blade has to do several materials |
| Other heights to order | set by request | Trim grade for tile and thin slab, or a taller grade for daily contractor work, arranged with the factory |
The price gap between a short segment and a tall one is small next to the gap in metres of cut, so the figure that matters is cost per metre. An 8 mm segment on a granite worktop is the balanced choice for a fabricator who also cuts marble and the odd brick; a shorter grade suits a shop that only trims tile. Tell us the material mix and we will confirm the height that fits the job.
Maximum rpm and Machine Match
Every diameter has a speed above which the rim is travelling past what the bond can stand, and the number on the label is a limit, not a target. The figure comes from peripheral speed: 80 metres per second at the rim, so rpm falls as the circumference grows.
| Diameter | 100 | 115 | 125 | 150 | 180 | 200 | 230 | 250 | 300 | 350 |
|---|---|---|---|---|---|---|---|---|---|---|
| Max rpm | 15,300 | 13,300 | 12,200 | 10,200 | 8,500 | 7,600 | 6,600 | 6,100 | 5,100 | 4,400 |
The sizes sort themselves in practice. A 100 or 115 mm grinder turns about 11,000 rpm, below the 15,300 and 13,300 limits. A 125 mm grinder runs 10,000 to 11,000, just inside 12,200. From 180 mm up the blade belongs on a bench or masonry saw with water, not in a hand.
Two rules follow. Never fit a blade larger than the machine was built for, because the machine will spin it at the smaller blade’s speed and the rim will be over its limit. And never run a blade above the rpm printed on it, however slow the cut feels, because the failure is the rim letting go rather than the blade wearing out.
Wet Cutting and Dry Cutting
This blade is rated for both, and the job usually decides. Water buys segment life, a cleaner edge and no dust. Dry buys a faster set-up and work where a hose is not going to happen. The protect teeth make dry work safer for the core, but they do not remove the reason to keep passes shallow.
Running wet
Water wants to arrive where the rim enters the stone, not sprayed over the guard. Three to five litres a minute is enough on a 125 to 180 mm blade, and the flow should be steady enough that the slurry leaves the cut milky rather than thick. On a tile saw the pump and tray do it for you; on a grinder it means a bottle and a second pair of hands, and it is worth the trouble.
Running dry
Dry cutting on granite works, but it is a technique rather than a switch. Take about 10 mm a pass on a 30 mm slab instead of plunging, let the blade spin free for ten or fifteen seconds between passes, and keep the feed steady. Listen as well: a blade that is cutting has a flat note, a blade that is rubbing climbs in pitch. If the cut starts to steer, stop and restart rather than levering, because levering is what bends a core.
The protect teeth are what make dry cutting reasonable here. A plain rim of the same thickness loses tension sooner, dishes and binds. The side teeth keep the core off the wall of the cut and interrupt that spiral, but they do not remove the reason to keep passes shallow or to let the blade cool between them.
Arbor, Bushing and Flange
The arbor is the bore in the middle of the blade, and it has to match the machine spindle exactly. Three sizes cover most of the world: 22.23 mm, which is 7/8 inch and the standard on angle grinders and tile saws; 20 mm, common on European and Asian machines; and 16 mm, used on small 100 and 115 mm grinders and marble cutters.
Bushings: pressed, not loose
A reducing bushing takes a 22.23 mm bore down to 20 mm or 16 mm, and it has to be a press fit in the blade and a close fit on the spindle. A loose bushing is the commonest cause of a blade that will not run true: a few tenths of a millimetre of play at the centre becomes visible swing at the rim, the blade cuts a curve, one side of the segment does all the work, and the rim wears into a taper no adjustment will correct.
Flanges and mounting
Both flange faces have to be clean, flat and free of burrs, and the flange has to be large enough to support the disc. Dirt on one face tilts the blade by more than the protect teeth can absorb, and the symptom is a blade that cuts well for a metre and then wanders. On a used machine, check spindle runout before blaming the blade.
Matching the Blade to the Material
The blade is one specification, so what is left to choose is segment height, mode and feed. The table is the short version of how those get assigned.
| Material | Segment height | Mode | What to expect |
|---|---|---|---|
| Granite, slabs and worktops | 8 mm | Wet preferred | Hard and abrasive. Steady feed, full water, and the rim lasts. Dry cuts work in 10 mm passes |
| Marble and soft stone | 8 mm | Wet | Cuts quickly and the rim barely works. Dry cutting risks heat marks on the face |
| Hard stone and quartz | 8 mm | Wet | Resin binder on quartz. Heat ruins the cut edge, and the dust is the one to avoid |
| Masonry, brick, block | 8 mm | Either | Abrasive and often reinforced. Ease the feed where the rim meets steel |
| Sandstone and limestone | 8 mm | Either | Very abrasive, so the segment wears quickly whatever you do. Expect short life |
| Porcelain and tile | 8 mm | Wet | Works with a slow feed and full support under the tile. A finer bond chips less |
Two patterns run across the table. Hard dense material wants water and a steady feed, because the diamond does the work and heat is the enemy. Abrasive material consumes segment height before it dulls the diamond, so a taller segment than the job needs buys nothing. The protect teeth help on every line here, because a square slot wall matters in masonry as much as in granite.
Troubleshooting
| Symptom | Usual cause | What to do |
|---|---|---|
| Rim looks polished and the blade stops cutting | Glaze: feed too light, or the material is softer than the bond was made for | Open the rim on an abrasive block for 20 to 30 seconds, then keep the feed up |
| Chips along the exit edge of a granite cut | Feed too fast, water off, or a glazed rim skating rather than cutting | Slow the feed, restore the water, dress the rim before the next cut |
| Slot wall ragged or the blade wanders | Protect teeth worn flat, or a loose bushing and dirt on the flange | Retire the blade if teeth are gone; else clean the flanges and fit a pressed bushing |
| Blade wobbles from the first cut | Missing or loose bushing, dirt or a burr on the flange | Clean both flange faces, fit a pressed bushing, check spindle runout |
| Cut curves away from the line | Rim worn to a taper, often from running a loose bushing | Replace the blade. A tapered rim cannot be dressed back straight in the field |
| Blue or straw colour on the core | Overheated from dry cutting with too deep a pass | Water, or 10 mm passes with a free run between them. A blue core has lost tension |
| Segment separates from the core | Cutting past the segment so the weld runs on stone, or sustained overheating | Replace at about 1.5 mm of segment. This is a wear limit, not a repairable fault |
| Loud ring or howl in the cut | Blade not supported by the flange, or a core that has lost its flat | Check flange diameter and flatness first, then replace the blade |
| Cut closes and grips the blade | Deep cut in a material that relaxes, or the blade is being levered | Step cut, use a wedge behind the cut, and keep the machine square to the line |
Frequently Asked Questions
- What is a turbo rim diamond blade with protect teeth?
- It is a continuous turbo rim blade with small diamond teeth standing proud on the side faces of the rim as well as the cutting face. Ten diameters cover 100 mm to 350 mm. The continuous rim keeps contact with the stone for a smooth, chip-free cut, and the side protect teeth square the wall of the slot and keep the core plate from rubbing on the sides of the cut. Segment height is 8 mm and the blade runs wet or dry.
- What are protect teeth and what do they do?
- Protect teeth are short segments welded to the side of the rim, proud of the steel core, so they touch the wall of the cut before the core does. In a plunge or a deep slot they dress the wall square and stop the nibble you get from a rim that only cuts on its face. They also take the side load off the core plate, which otherwise heats and dishes where it rubs. On a blade rated for both wet and dry work, that side protection is what keeps the disc true after a long dry run.
- Why a continuous turbo rim rather than separate segments?
- A turbo rim is a single band with a waved edge pressed into it, so the diamond is in the cut the whole way round. The cut stays smooth because the rim never leaves the stone the way a segmented blade does between gullets, and the exit edge of a granite slab comes away clean rather than scalloped. The wave in the rim does the clearing work that gullets would otherwise do: it carries water in and swarf out so the bond keeps wearing back and fresh diamond keeps coming up.
- What segment height should I order?
- This blade is built on an 8 mm segment as standard, which gives about 6.5 mm of usable band above the steel before the blade is at its wear limit. Eight millimetres suits mixed stonework, granite and masonry where one blade has to do several jobs. Other segment heights are arranged to order for distributors who want a trim grade or a longer life grade, and the height changes neither the diameter nor the segment width. Tell us the material and the machine and we will confirm the height that fits.
- Can this blade cut granite dry?
- Yes, the blade is rated for dry cutting and the side protect teeth keep the core from rubbing as it heats, but dry granite wants discipline. Take 10 mm passes on a 30 mm slab instead of one plunge, let the blade run free for ten or fifteen seconds between passes, and stop the moment the cut starts to steer. Dry cutting costs segment life and it puts respirable silica in the air, so water or extraction is the better default indoors. The protect teeth buy you a straighter dry cut, not a free pass to overheat the core.
- Will it cut porcelain tile without chipping?
- It will, with a slow feed and water, but a continuous rim blade with a finer bond is the better tool for porcelain. This blade is built around granite and hard stone, where a fine bond would glaze. On porcelain, support the tile right up to the cut line, use water, and let the blade cut rather than pushing it through. Chipping at the exit edge is nearly always feed rate, not the blade, and the smooth turbo rim here is more forgiving than a coarse segmented edge would be.
- What arbor do I need and can you supply a bushing?
- The 100 and 115 mm blades come in 16, 20 or 22.23 mm; the 125 and 150 mm in 20 or 22.23 mm; from 180 mm up in 22.23 or 25.4 mm. 22.23 mm is 7/8 inch, the common angle grinder and tile saw bore. 20 mm suits most European and Asian machines, 16 mm the small marble cutters, and 25.4 mm bench and masonry saws. Reducing bushings are supplied with the blade on request and are pressed in, not loose, so the disc runs true from the first cut.
- What is the maximum rpm for each diameter?
- It is set by peripheral speed, and for a diamond blade the rated figure is 80 metres per second at the rim. That gives 15,300 rpm at 100 mm, 13,300 at 115 mm, 12,200 at 125 mm, 10,200 at 150 mm, 8,500 at 180 mm, 7,600 at 200 mm, 6,600 at 230 mm, 6,100 at 250 mm, 5,100 at 300 mm and 4,400 at 350 mm. The figure is printed on the blade; never run a blade above the marking, and never fit a blade larger than the machine was built for.
- Why did my blade glaze and stop cutting?
- Glaze is a polished rim: the diamond is still in the bond but blunt, and the metal around it has been rubbed smooth instead of wearing back. It comes from feed that is too light for the material, from cutting something softer than the blade was bonded for, or from running without enough water. Open the rim again on an abrasive block or a piece of sandstone for twenty or thirty seconds, then keep the feed up so it does not happen a second time. The turbo wave in this rim clears the bond more readily, though it still needs a real feed.
- How long does the segment last?
- Segment life is quoted in linear metres of cut, not in hours, because the blade wears per metre of stone. As an industry reference, an 8 mm segment on a 125 mm blade gives roughly 50 to 100 m of 20 mm deep cut in granite, less in engineered quartz, more in marble and soft limestone. Feed rate moves that figure more than anything else: a blade that is pushed wears the segment out sooner than one that is allowed to cut. Abrasive masonry shortens life whatever the feed, because the stone eats the bond.
- Will one blade work on both an angle grinder and a tile saw?
- If the arbor and the speed match, yes. A 125 mm blade with a 22.23 mm bore fits both a 125 mm grinder and most 125 mm tile saws, and the saw will run it slower and wetter, which suits granite. Check the machine spindle speed against the blade marking first: a tile saw that turns slower than the blade is rated for is fine, one that turns faster is not. The protect teeth help on the saw too, because a square slot wall matters as much in a wet cut as a dry one.
- What is the minimum order and can you print my brand?
- Minimum order is 100 pieces per size, and mixed sizes in one order are accepted so a distributor can build a range. Lead time is 20 to 30 days after the artwork and the specification are confirmed. We print your logo and grade on the label, supply the blade with your own sleeve or blister, and hold the same bond and diamond specification from order to order so a re-order behaves like the first. The protect teeth profile and the 8 mm segment are held constant across the range.