1. Our own copy: the claim that cannot be true
Three sentences in the source description do real damage, and one of them is a straightforward impossibility. It is worth putting them side by side, because a buyer who has already read them arrives with the wrong mental model of the product.
| What the source copy says | What is wrong | What we say instead |
|---|---|---|
| “by using a standard coring drill bit, you can create many different hole sizes without having to purchase several different coring drills” | Physically impossible. The hole is the tube’s outside diameter. Nothing on a core bit is adjustable, and re-running the same bit in the same hole only polishes it | One bit, one diameter, permanently. This is exactly why sets exist — section 2 |
| “used for dry/wet drilling and beveled tiles” | A bevel is an edge profile, not a material. Listing it as a workpiece category tells the reader the page was not written by someone who drills tile | Through-body porcelain, glazed ceramic, granite, marble, engineered stone, brick and block. Bevel is irrelevant to drillability; body density is not |
| “A boxed set can meet most daily needs” | “Daily needs” is not a specification. Needs are a list of holes with diameters, and a set either covers them or does not | Write the hole list first, then choose the set. Section 4 and section 5 |
The first error has a commercial consequence that is easy to miss. A buyer who believes one bit can make several sizes will buy the smallest useful set, discover on site that they cannot open a 28 mm hole with a 20 mm bit, and conclude that the tool is bad rather than that the purchase was. The page should not set that trap.
2. One bit, one diameter — what “core” means
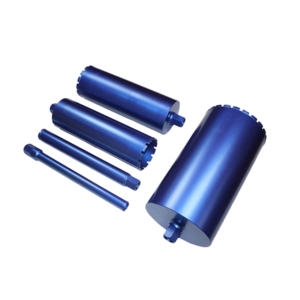
“Core” describes the geometry of the cut, not the material. A core bit is an annular tool: it cuts a ring of material and leaves the centre intact. That is why it can open a 100 mm hole in porcelain with a fraction of the contact area, spindle load and heat of a 100 mm solid bit — and it is also why the hole it makes is fixed.
| What the tool is | What it means when you buy a set |
|---|---|
| A tube, not a drill. Diamond on the rim, steel wall behind it, an open bore up the middle | The outside diameter of the tube is the hole. There is no adjustment, no expanding jaw, no collet. A set is a list of diameters because it has to be |
| An annular cut. It removes a ring and leaves a plug | The plug is the second failure point. A perfect hole can still end with a chipped edge if the plug is levered out against the tile face |
| No centre point. Unlike a hole saw there is no pilot drill in the middle | The rim has to be started at an angle to score the glaze, or guided by a plate or a template. A core bit with no start control skates on glazed tile |
| Thin wall, around 1 to 2 mm. Thin by design, because the tool only has to remove a ring | It cuts fast and cool, and it is fragile. A bent barrel from a drop or a levered cut drills an oversized hole for the rest of its life, and it cannot be straightened |
| Grit on the face and a short band up the wall. Above the band the tube is bare steel | Below the band the tool cuts; above it, bare steel runs in the hole. That is why water, wax and feed control matter, and why a deeper hole needs a different tool rather than more force |
| A threaded connection, not a shank. M14 or 5/8-11 UNC, or a hex adapter | The connection is a standard, and it is a market decision rather than a technical one. Section 8 |
The practical consequence is the one buyers resist: there is no such thing as “drilling it a bit bigger” with a core bit. If the hole is undersized, the only fix is the next diameter up, and that second cut has no centre to guide it. That is precisely the situation where a hole drifts, the trim stops covering it, and a tile comes off the wall. The sizing decision has to happen before the first hole.
This is also the cleanest way to tell a core bit from the tools around it in the catalogue. A non-core diamond bit is a solid-bodied tool for a different kind of work; a hole saw looks similar in a photograph but carries a pilot drill and an arbor, and the pilot is what a core bit deliberately does not have. If you want the single-bit version of this product rather than a box, that is the diamond core drill bit set and the vacuum brazed single-bit set, and the construction argument behind both is set out on the vacuum brazed core drill bits set page.
3. 60 mm long is 35 mm deep
This is the number that catches almost every buyer. The bit is described as 60 mm long, and it is — but the last 25 mm of that length is thread socket and the shoulder the arbor seats against, and none of it can enter the hole. The cutting depth is what is left.
| Size band | Diamond band height | Overall length | Published maximum working depth | What the difference is |
|---|---|---|---|---|
| 6–16 mm | 10 mm | 60–62 mm | 35 mm | About 25 mm of thread socket and seating shoulder that stays above the work |
| 19 mm and above | 15 mm | 75 mm | 50 mm | The same 25 mm, on a longer barrel |
The consistency is the point. Specifications published by several independent suppliers give the same pairs — 60 mm length with 35 mm depth, 62 mm with 35 mm, 75 mm with 50 mm — and in every case the difference is 25 mm. That makes it a design constant of the format rather than one factory’s choice, which is why it can be written as a rule:
Two consequences follow, and the second one is the one nobody expects.
The depth is not uniform across a set
The small bits — 6, 8, 10, 12, 16 mm — are the ones used for pipe, cable and fixing penetrations, and they are 15 mm shallower than the large ones in the same box. A 68 mm bit will go 50 mm; a 10 mm bit from the same set will go 35 mm. Buyers assume the opposite, because a bigger bit looks like a bigger job.
What that means on a real wall
| Job | Material stack | Depth needed | Verdict on a 6–16 mm bit (35 mm) |
|---|---|---|---|
| Wall tile on cement board | 10 mm tile + 12 mm board | 22 mm | Fine — comfortable margin |
| 20 mm porcelain slab on adhesive | 20 mm slab + 10 mm adhesive | 30 mm | Fine, but only 5 mm of margin |
| Slab on a thick bed with a membrane | 20 mm + 15 mm + 2 mm | 37 mm | Past the limit — needs a long-shank bit |
| Brick veneer with a cavity | 20 mm brick + 50 mm cavity | 70 mm | Wrong tool — this is a masonry core job |
If a job needs more depth than the band allows, the answer is not a bigger diameter from the same set and it is not more pressure. It is a long-shank diamond core drill bit, which extends the barrel rather than the thread. The same distinction separates this tool from a segmented core bit, where the diamond sits in a segment on the end of a long barrel and depth is limited by barrel length rather than by a brazed band.
4. Size the hole from the fitting, not from the ladder
The hole is not chosen because it is the next size in the box. It is chosen because something has to pass through it. Start from the pipe, valve or drain, take its outside diameter, and add clearance.
The clearance is not cosmetic. Tile is brittle and a building moves. If the pipe is clamped hard against the edge of the hole, any movement of the plumbing loads the tile directly and the crack runs out from the hole. A few millimetres of gap, hidden by the escutcheon or flange, is what stops that. It is also what allows the pipe to be centred in the hole rather than forced to one side.
| What passes through the tile | Pipe outside diameter | Hole to drill | Nearest ladder size | Note |
|---|---|---|---|---|
| 1/2 in copper or PEX supply, toilet or sink stub | 15.9 mm (5/8 in) | 22.2 mm (7/8 in) | 20 mm or 25 mm | Neither is exact — you are rounding on every hole |
| 3/4 in copper or PEX | 22.2 mm (7/8 in) | 28.6 mm (1-1/8 in) | 28 mm | The one common plumbing size that does land on a metric ladder |
| 1/2 in threaded pipe: shower arm, tub spout | 21.3 mm (0.84 in) | 28.6 mm (1-1/8 in) | 28 mm | Check the escutcheon before drilling — some trims need more |
| Mixer or valve body | Varies by valve | 35–50 mm | 35 / 40 / 45 / 50 mm | Read the valve instructions; the trim plate sets the hole, not the pipe |
| 1-1/2 in PVC or ABS drain | 48.3 mm (1.90 in) | 54–63.5 mm | 55 mm or 60 mm | Drain flanges usually cover a generous gap |
| 2 in PVC or ABS drain | 60.3 mm (2.375 in) | 69.9 mm (2-3/4 in) | 68 mm | At this size the plug is heavy and the break-out needs care |
The metric ladder was built for fasteners, not for pipes
Look down the “hole to drill” column: 22.2, 28.6, 34.9, 54.0, 63.5, 69.9 mm. Those are inch numbers, because plumbing is an inch trade. The set offers 20, 25, 28, 30, 35, 40, 45, 50, 55, 60, 68 mm, because the ladder follows fixing and anchor practice. Only 28 mm comes close enough to count as a match, and even that is 0.6 mm under the nominal hole.
So every plumbing hole on a metric ladder is a decision to round down or round up, and the two are not equally safe:
- Round down and the pipe may not fit, or fits with the tile touching it. A tight fit converts plumbing movement into a load on the tile.
- Round up and the hole is larger than the pipe needs. That is fine as long as the trim covers it — which is the arithmetic in section 7, and it has a hard limit.
This is why the trim should be chosen before the hole is drilled, not after. A shower valve trim plate and a 40 mm decorative escutcheon have very different appetites for a mistake.
5. Count versus coverage: real set compositions
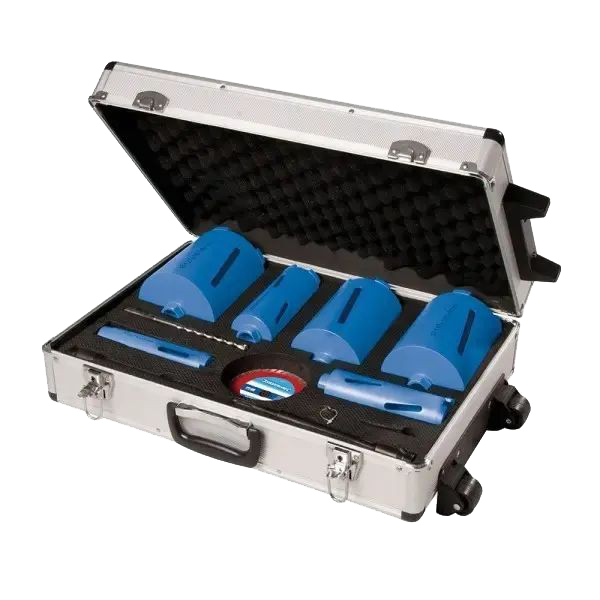
Sets in this category are not arbitrary. The same compositions recur across suppliers, and reading them shows what the market is actually buying. Here are five configurations that exist in the trade, scored by the holes they can make at the correct size rather than by how many pieces are in the box.
| Set | Sizes in the box | Pieces | Anchors 6–12 mm |
Small services 16–35 mm |
Drains 45–68 mm |
Large 100 mm |
Verdict |
|---|---|---|---|---|---|---|---|
| A | 6 / 8 / 10 / 12 + adapter | 5 | Yes | No | No | No | Fixing set only. No plumbing at all |
| B | 20 / 35 / 40 / 50 / 68 | 5 | No | Partial — no 25 or 28 | Yes | No | Looks like a plumbing set; misses the two commonest plumbing sizes |
| C | 20 / 25 / 30 / 35 / 40 / 50 / 60 / 68 | 8 | No | Partial — no 28 | Yes | No | Better than B, still cannot hit a 3/4 in line exactly |
| D | 6 / 8 / 10 / 12 / 20 / 25 / 28 / 35 / 45 / 50 / 68 + adapter | 11 | Yes | Yes | Yes | No | The first genuinely mixed set that covers both ends |
| E | 6 / 8 / 10 / 12 / 16 / 20 / 25 / 30 / 35 / 45 / 55 / 68 / 100 | 13 | Yes | Yes | Yes | Yes | Full range, and it is the only one with 16 mm and 100 mm |
Three things fall out of that table, and all three contradict the way sets are usually sold.
Two five-piece sets can be disjoint
Set A and Set B have the same piece count and almost no overlap. A customer who buys on count alone has a fifty-fifty chance of buying the wrong half of the range. The number of pieces is not a measure of coverage; it is a measure of how many boxes the factory had.
The 8-piece can be less useful than the 11-piece
Set C has eight bits and still cannot drill a 28.6 mm hole for a 3/4 in line at the correct size. Set D has eleven and can. Counting pieces would rank them the wrong way round for the job that matters most in a bathroom.
The gap is not where you think
Set B has 20, 35, 40, 50, 68 — a gap from 20 to 35 that contains 25, 28 and 30, three sizes that matter. It also has no 16. The visual impression of a set is created by its largest and smallest bits; the gap that costs a job is almost always in the middle, where nobody looks.
6. The gaps that cost the job
Not every missing size matters. A missing 55 mm is an inconvenience; a missing 28 mm stops a bathroom. The difference is whether the size corresponds to something that actually has to pass through a wall.
| Transition in the ladder | What lives in the gap | If you do not have it | Cost |
|---|---|---|---|
| 12 → 20 mm | 14 mm (M12 fixings), 16 mm (5/8 in shower arm, some anchors) | Jump to 20 mm | High — 20 mm around a 16 mm pipe leaves a 4 mm gap per side, usually coverable, but 20 mm around a 14 mm fixing may not be |
| 20 → 35 mm | 25, 28, 30 mm — 3/4 in supply, shower arms, smaller valve bodies | Jump to 35 mm | Highest — this is the most common plumbing range and the gap is widest here |
| 35 → 45 mm | 40 mm — small valve bodies, some wastes | Jump to 45 mm | Moderate — trim usually covers, but the pipe is no longer centred |
| 68 → 100 mm | 75 mm, 90 mm — large wastes, ducting, downlights | Jump to 100 mm | High — 100 mm is past most trims and past the practical limit of a hand-held cut in porcelain |
The asymmetry between the two failure directions is the thing to hold on to. An undersized hole stops the job; an oversized hole ends the finish. An undersized hole cannot be fixed with the bit in your hand, because a core bit will not enlarge an existing hole — it has no cutting edge on the inside and no centre to guide it. An oversized hole cannot be fixed at all: the tile has to come off.
That sounds like an argument for always going up a size, and it is not, because the oversized direction has a limit that is measured in millimetres and printed on the trim. Section 7 is that limit.
One practical exception: if a set has a gap you cannot avoid, buy the missing size as a single bit rather than stepping up. A single vacuum brazed core drill bit in the gap size costs less than the tile you would lose, and it keeps the rest of the set honest.
7. The cover budget: how far you can over-drill
An escutcheon, flange or trim plate is the only thing standing between a slightly oversized hole and a visible defect. It has to overlap the hole, not merely reach its edge, so there is a hard arithmetic limit on how far up the ladder you can go.
The 10 mm is 5 mm of overlap on each side, which is about the minimum that looks deliberate rather than lucky and that survives a little movement. A 60 mm decorative escutcheon covers a 50 mm hole. A 72 mm split flange covers about 62 mm. A 150 mm shower valve plate covers far more than any bit in the set, which is why valve holes are forgiving and pipe holes are not.
| Trim outside diameter | Largest hole it covers | Biggest ladder size that fits | Typical use |
|---|---|---|---|
| 45 mm | 35 mm | 35 mm | Small decorative collar on a 1/2 in stub |
| 50 mm | 40 mm | 40 mm | Compact escutcheon, tight to a wall |
| 60 mm | 50 mm | 50 mm | Standard decorative escutcheon |
| 72 mm | 62 mm | 60 mm | Split flange, floor and ceiling plate |
The example that goes wrong
A 22 mm pipe in a visible field, drilled with the 68 mm bit because it was the only one in the box near the right size. The gap is 23 mm on every side. A 60 mm escutcheon has a 30 mm radius and the hole has a 34 mm radius, so the trim cannot reach past the edge of the hole at all. There is no adjustment, no sealant trick and no rotation that fixes it. The tile comes off.
Set against that, the same 68 mm bit used for a 2 in drain with a 0.84 in flange opening is correct, because the pipe fills the hole and the flange is doing the job it was designed for. The bit is not the error; the pairing is.
8. The thread is a market decision
A core bit does not have a shank, it has a thread. That matters more for an exporter than for a user, because the same bit cannot be sold into both major markets without either a second thread option or an adapter in the box.
| Connection | Where it is the native standard | What the machine is | What the buyer needs |
|---|---|---|---|
| M14 | Europe | Angle grinder with an M14 spindle | Nothing extra if they own a grinder |
| 5/8-11 UNC | North America | Angle grinder with a 5/8-11 spindle | Nothing extra if they own a grinder |
| Hex adapter | Anywhere a drill or driver is used | 3/8 in hex in a three-jaw chuck | An adapter, which adds a joint and about 55 mm between chuck and rim |
Three practical points that the packaging rarely makes clear:
- The threads do not interchange. M14 is a metric coarse thread; 5/8-11 UNC is an inch thread. They will not engage, and forcing them damages both the bit and the spindle.
- An adapter is a joint, not a conversion. Every joint between the spindle and the rim adds run-out, and run-out drills an oversized hole. For occasional work it is fine; for daily work it is the wrong purchase.
- The adapter does not change the bit’s depth. The 25 mm of socket and shoulder in section 3 is inside the bit and stays inside it. The adapter adds length on the machine side, which reduces reach and stiffness, not cutting depth.
For a set, state the thread on the order line and state it again on the box. A mixed pallet of M14 and 5/8-11 sets that is not labelled per carton will produce returns that are impossible to argue, because from the outside the two look identical.
9. Running it: the start and the plug
Most of the technique for this tool is about heat, and that mechanism is on the vacuum brazed core drill bits set page: the braze alloy softens and the diamond degrades long before the steel body would care, so water is a requirement rather than an option, and the wax in the small sizes is a starting charge rather than a cooling system. What is specific to a set is the two moments that ruin a good hole: the entry and the plug.
The entry
A core bit has no centre point, so a flat start on glazed porcelain skates. The standard technique is right and worth repeating: start with the rim at about 45 degrees to the surface, at low speed, with water already running, until it has cut a shallow crescent; then bring the bit upright and continue. The crescent becomes the guide that the pilot would have provided.
If the hole is in a visible field, tape the surface first. The most common way a tile is ruined is not a bad hole, it is the bit skating off the mark and scoring a line across the glaze that will not polish out.
The plug
Because the cut is annular, the centre stays as a disc. It has to be removed, and this is where a hole that was perfect for thirty seconds ends up chipped. Do not lever against the tile face. Drill until the rim just breaks through, ease the feed, and take the plug out from the back, or through the bore with a thin tool. On a wall, a small relief hole beside the plug makes the break-out controllable.
Two constraints that are not about technique
- Never use hammer mode. The impact that helps a masonry bit shatters tile. Confirm the machine is in rotary-only before the rim touches the surface.
- Stay about 25 mm from a tile edge where you can. A hole near an edge has nothing on one side to carry the stress, so the same hole is far more likely to split the tile. With a mixer valve you often have no choice; slow down as the rim reaches the edge.
10. Full specifications
| Tool type | Annular diamond core bit, single-layer vacuum brazed, supplied as a boxed set of diameters |
|---|---|
| Standard diameters | 6, 8, 10, 12, 14, 16, 20, 25, 28, 30, 32, 35, 40, 45, 50, 55, 60, 65, 68, 75, 100 mm; other sizes on request |
| Small size band | 6–16 mm: diamond band 10 mm, overall length 60–62 mm, maximum working depth 35 mm |
| Large size band | 19 mm and above: diamond band 15 mm, overall length 75 mm, maximum working depth 50 mm |
| Working depth rule | Overall length minus about 25 mm of thread socket and seating shoulder |
| Wall thickness | Approximately 1–2 mm, thin by design |
| Diamond grit | 35/40 as standard; 40/50 and 50/60 on request |
| Connection | M14 (Europe) or 5/8-11 UNC (North America); hex adapter available |
| Adapter | M14 male thread to 3/8 in hex shank, about 55 mm overall, 28 mm shank length |
| Core form, small sizes | Wax-filled for dry starting and short runs |
| Core form, large sizes | Open core with chip clearance; water strongly recommended |
| Cutting geometry | Diamond on the face plus a band up the wall; above the band the tube is bare steel |
| Suitable materials | Porcelain and ceramic tile, glazed tile, granite, marble, engineered stone, brick, block, light concrete |
| Marginal | Glass (chipping risk, needs very light feed and continuous water), heavily reinforced concrete |
| Not suitable for | Structural concrete at depth, steel, wood, plastics, hammer mode |
| Typical set sizes | 4, 5, 8, 11 and 13 piece configurations; custom assortments on request |
| Packaging | Blow-moulded case; sizes marked per bit; barcode and insert card to your artwork |
| OEM / ODM | Case colour, label, laser marking and size assortment to order |
Stock versus special. The diameters above are the common range; the composition of the set is a separate decision from the diameters in it. A customer can order any assortment of standard diameters as a set, which is usually the cheapest way to solve a coverage gap without buying a second box.
11. What to put on the purchase order
Most wrong shipments in this category are not manufacturing errors. They are orders that specified a piece count instead of a coverage list. A set order should read like a specification, not like a catalogue line.
| Field on the order | What to state | Why it matters |
|---|---|---|
| The hole list | The services that have to pass through: 1/2 in supply, 3/4 in supply, shower arm, mixer, 1-1/2 in waste | This is what defines coverage. The piece count follows from it, not the other way round |
| Diameters | Every size, in millimetres, with the inch equivalent in brackets | Removes the metric-versus-imperial rounding argument before production |
| Depth requirement | The thickest stack the bit must pass, in millimetres | If it exceeds 35 mm on a small size, the order needs long-shank bits rather than a bigger diameter |
| Thread standard | M14 or 5/8-11, per destination market | Not interchangeable; a wrong thread is a whole-carton return |
| Adapter | Included or not, and which shank | Determines whether the set works on a drill as well as a grinder |
| Core form | Wax-filled or open, per size band | Affects the cooling instructions printed on the insert |
| Marking | Size laser-marked on every bit, not only on the case | Loose bits in a site box are otherwise unidentifiable, and a set becomes a pile |
| Spares | Extra units of the two most-used sizes | The small sizes wear first because they are used most; a set with no spare 6 and 8 mm stops early |
12. Incoming inspection
A set is harder to inspect than a single bit, because a defect in one diameter is easy to miss when twelve others are correct. Check the sizes you will use most, and check them by measurement rather than by eye.
| Check | Method | Accept / reject |
|---|---|---|
| Outside diameter | Caliper at three points around the rim, on every size you will use | Reject a size that is out of round or outside the stated tolerance; an oval tube drills an oval hole |
| Diamond band height | Measure the coated band up the wall with a rule or caliper | Should match the band for that size class (10 mm small, 15 mm large). A short band is a short-life bit sold as full |
| Braze coverage | Look at the rim under good light, all the way round | Reject bare patches or a rim where grit is sparse on one side; that side will wear first and the hole will drift |
| Thread | Thread gauge, or screw onto a known-good arbor | Reject cross-threading, burrs or a thread that bottoms before the shoulder seats |
| Run-out | Mount on a known-good arbor, spin by hand against a fixed point | Visible wobble means a bent barrel or an off-axis thread; both drill oversized holes |
| Barrel straightness | Roll on a flat surface | Reject any bit that does not roll true. A bent core bit cannot be straightened |
| Marking and case | Size on every bit, case insert matches the assortment | Reject mismatched inserts; they cause a wrong-size hole on site more often than a bad bit does |
13. Troubleshooting
| Symptom | Most likely cause | What to change |
|---|---|---|
| Hole is oversized from the first cut | Skating start, bent barrel, or run-out from an adapter joint | Score a crescent at 45 degrees before going upright; reject a bent bit; remove the adapter if you can |
| Chips at the entry | Started dry, or flat at speed, or in hammer mode | Water before contact, angled start, rotary only |
| Chips at the exit | Feed not eased as the rim breaks through, or unsupported back face | Ease the feed at breakthrough; support or back up the exit face |
| Bit stops cutting and the rim looks shiny | Grit is gone; the steel is rubbing | Replace the bit. There is no resharpening that brings diamond back |
| Bit grabs as it crosses a grout line | Grout is softer than tile, so the rim snatches at the transition | Move the hole into one tile if possible; if not, slow down and lighten the feed at the joint |
| Plug will not come out | Drilled past the core, or the plug is wedged and dry | Break it out from the back; add water; never lever against the tile face |
| Bit will not fit the arbor | Wrong thread standard, or a damaged first thread | M14 and 5/8-11 are different standards; check before forcing |
| Burning smell or steam off the cut | Too fast, too dry, or a blocked groove | Water on, slower, clear the kerf; the wax charge is already spent |
14. Applications
- Bathroom and kitchen tile: pipe penetrations, shower arms, mixer valves, wastes. The core of the market for a mixed set.
- Stone and engineered stone countertops: faucet holes, soap dispenser holes, cable grommets. Slab thickness makes the depth check essential.
- Porcelain and ceramic wall tile: anchor and fixing holes at 6–12 mm, where the small sizes earn their place.
- Marble and granite: clean holes without the edge chipping a percussion tool would leave.
- Brick and block: shallow penetrations for pipe and cable; not a replacement for a masonry core at depth.
- Light concrete: small diameters only, and not where reinforcement is expected. For structural concrete, the right tool is a concrete core drill bit.
- Glass: possible with a very light feed and continuous water, but not the application to buy this set for.
For work where the diamond is electroplated rather than brazed, the trade-offs are different again and are set out on the electroplated diamond core drill bit page. And where the job is wood rather than tile, a core bit is the wrong family entirely: the bi-metal hole saw set and the HSS hole saw set both cut timber with a pilot drill doing the locating that a core bit cannot do.
15. Frequently asked questions
Can one diamond core bit drill several different hole sizes?
No, and our own listing copy says it can, which is the most expensive sentence on the page. A core bit is a steel tube with diamond on the rim; the hole it makes is the outside diameter of that tube. There is no chuck, jaw or collet to adjust, no expanding mechanism, and no way to make the tube wider. Reaming a diamond-drilled hole with the same bit only polishes the wall. This is precisely why sets exist: one bit equals one diameter, so a set is a list of diameters, and the only useful question is which of your holes that list covers.
How many pieces do I actually need in a set?
The piece count tells you almost nothing. Start from the holes you have to make, not from the box. Write down every pipe, valve, drain, anchor and fixing that has to pass through the tile, convert each to a required hole diameter, then check which set covers those diameters without a gap. Two five-piece sets can cover completely different halves of the range, and an eight-piece set can be less useful than an eleven-piece one if the eleven has the size you need and the eight does not. A set is a coverage table; count the covered holes, not the tools.
What size hole do I drill for a 1/2 inch pipe in tile?
A half-inch copper or PEX supply has an outside diameter of about 15.9 mm (5/8 inch), and the hole is normally drilled at about 22 mm (7/8 inch). The rule used in the trade is roughly 6 mm larger than the pipe outside diameter, which is 1/8 inch of clearance on every side. The tile must never touch the pipe: contact turns any movement of the plumbing into a point load on the tile, and the crack starts at the hole. The gap is then hidden by the escutcheon, which is why the trim has to be chosen before the hole is drilled.
Why does a 60 mm long core bit only drill 35 mm deep?
Because the last 25 mm of the barrel can never enter the hole. The thread socket and the shoulder the arbor seats against sit at the machine end, and they stop at the surface of the work. Published specifications across several suppliers are consistent about this: a 60 to 62 mm bit is rated at 35 mm maximum working depth, and a 75 mm bit is rated at 50 mm. In both cases the difference is 25 mm. So the honest number to quote on a specification sheet is the maximum working depth, and the overall length is a packaging dimension, not a capability.
Why are the small bits in my set shallower than the large ones?
Because the two size bands are built on different barrels. The 6 to 16 mm bits are typically 60 to 62 mm long with a 10 mm diamond band and a 35 mm maximum working depth; the 19 mm and larger bits are about 75 mm long with a 15 mm diamond band and a 50 mm working depth. This is the reverse of what most buyers assume, because the small sizes are the ones used most often for pipe and cable penetrations. If your job needs more than 35 mm of depth at a small diameter, you need a long-shank bit rather than a bigger one from the same box.
Should I buy M14 or 5/8-11?
Buy the thread that matches the market you are selling into and the machine your customer already owns. M14 is the European connection and is native to angle grinders; 5/8-11 UNC is the North American connection and is also the grinder standard there. They are not interchangeable and no adapter makes them the same tool, because an adapter is an extra joint between the spindle and the rim, and every joint adds run-out. If you are shipping to both markets, stock both threads or state clearly which adapter is in the box.
Can I use an M14 bit on a 5/8-11 grinder?
Not directly. The threads are different standards and will not engage, and forcing them damages both the bit and the spindle. A thread adapter exists, but it adds a joint, increases the distance between the spindle and the cutting rim, and introduces run-out that shows up as an oversized hole. For occasional use it is acceptable; for daily work it is a false economy. The correct answer is to buy the bit with the thread your machine was built for.
Can I enlarge a hole with the same core bit?
No. A core bit has no pilot and no cutting edge on the inside of the tube, so running it in an existing hole does not enlarge the hole, it rubs the wall and generates heat. If a hole is too small you need the next diameter up, and the second cut will have no centre to guide it, which is exactly when a hole drifts and the trim stops covering it. This is why the sizing decision has to be made before the first hole, not corrected afterwards.
Why is there no 18 mm or 22 mm in the set?
Because the ladder was built for fasteners, not for pipes. Standard sets step through 6, 8, 10, 12, 16, 20, 25, 28, 30, 35 and so on, which follows fixing and anchor practice. Plumbing, however, produces inch-based hole sizes: 22.2 mm for a half-inch supply, 28.6 mm for three-quarter inch, 34.9 mm for a shower arm, 54 mm and 63.5 mm for drains. None of those land on the metric ladder, so every plumbing hole is a decision to round down and risk a tight fit or round up and rely on the trim. Know which way you are rounding before you drill.
How far can I over-drill before the trim stops covering it?
The escutcheon or flange has to overlap the hole by at least about 5 mm on every side, so the largest hole it can cover is roughly its outside diameter minus 10 mm. A 60 mm escutcheon covers a 50 mm hole; a 72 mm split flange covers about 62 mm. This is why going one size up is usually safe and going three sizes up is not. A 68 mm bit used for a 22 mm pipe in a visible field leaves a 23 mm gap per side, and a 60 mm escutcheon cannot reach across it, so the hole is unrecoverable.
What is the plug, and how do I get it out without chipping the tile?
A core bit cuts a ring, so the centre of the hole stays as a solid disc of tile attached to the substrate or loose in the bore. It has to be removed, and that is the second place a good hole gets ruined. Do not lever against the tile face. Drill until the rim just breaks through, ease off, and break the plug out from the back or through the bore with a thin tool. On a through-hole in a wall, drill a small relief hole beside the plug if the back is accessible. The plug is the reason a perfect hole can still end with a chipped edge.
Do I need a different bit for a 20 mm porcelain slab?
You need to check the depth, not just the diameter. A 20 mm slab on a 10 mm adhesive bed is a 30 mm stack, which is inside the 35 mm working depth of a small bit but with very little margin for a thick bed or a waterproof membrane. At 37 mm you are past the limit and need a long-shank core bit. Porcelain is also dense enough that the feed has to be steady rather than light, because a light feed polishes the grit instead of cutting it. Depth and density are two separate checks.
OEM & Wholesale
GUSHI supplies diamond core drill sets in custom assortments, with the thread standard, case artwork, size marking and insert card specified per market. Because the set composition is the product in this category, the assortment is treated as a specification rather than a stock choice: tell us the hole list and the destination market, and the sizes follow.