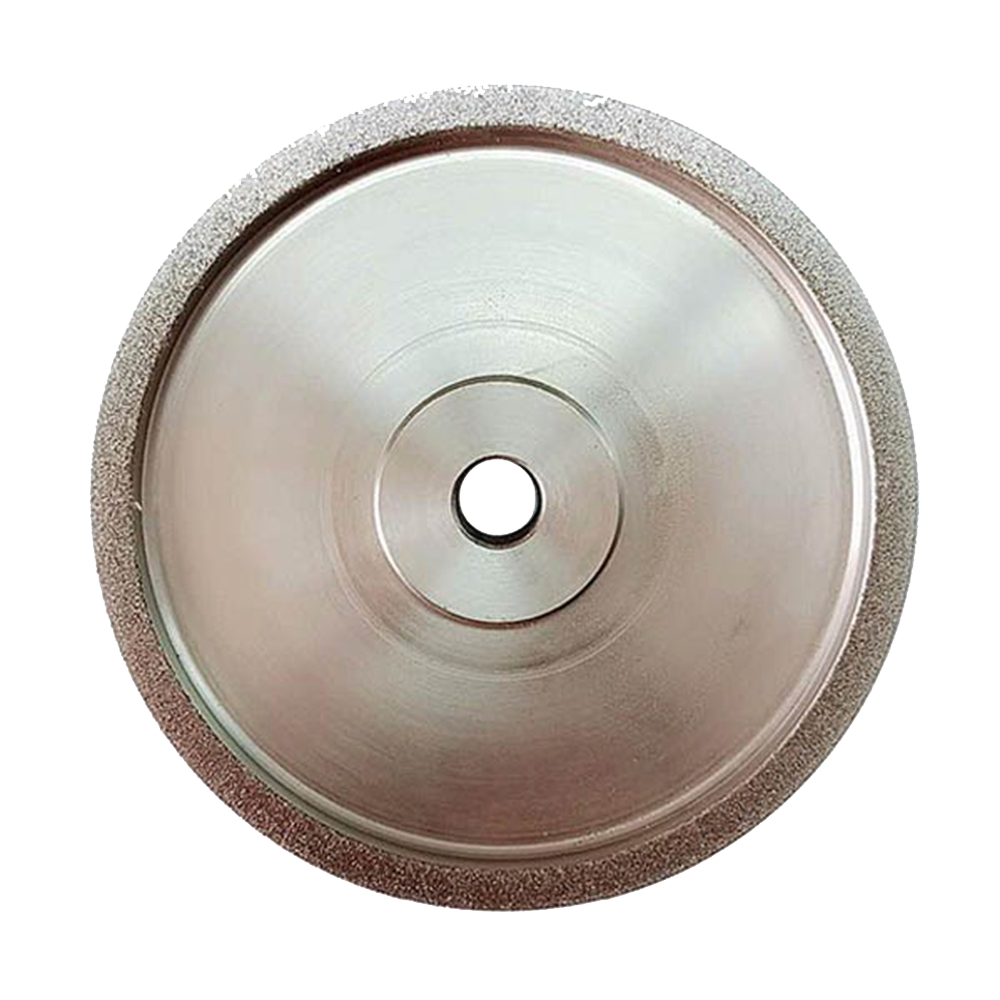
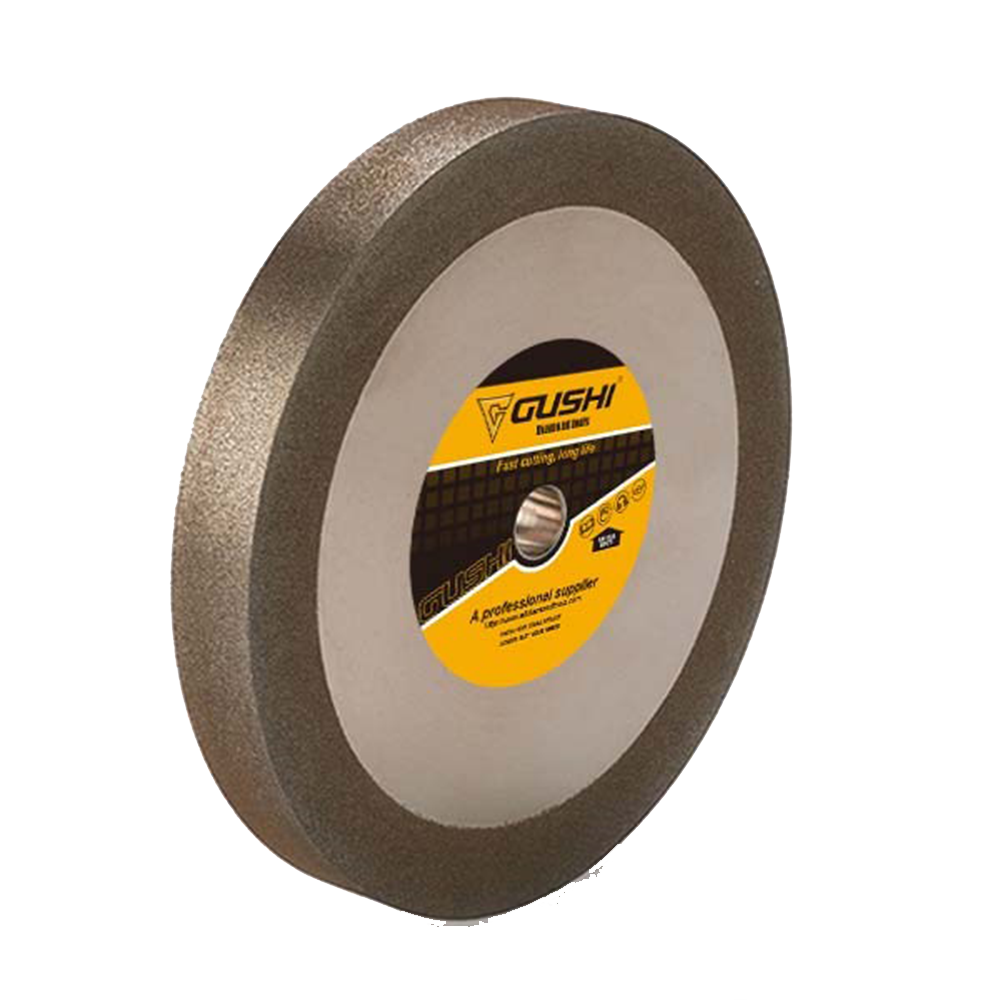
When you grind hardened steel, high-speed steel or die steel, the wheel you pick decides whether you get a mirror edge or a burnt one. GUSHI resin-bonded CBN (cubic boron nitride) grinding wheels are built for exactly that job.
CBN is the second-hardest abrasive after diamond, but unlike diamond it has no chemical affinity with iron — so it does not graphitize or burn away on steel. Combined with a resilient phenolic resin bond, the wheel cuts cool, self-sharpens as it wears, and holds a profile through thousands of parts.
The result buyers actually care about: a repeatable surface finish down to Ra 0.2 μm, far fewer dressing stops, and a wheel that simply lasts longer.
Why CBN — and Why Resin Bond
A grinding wheel is three things working together: the abrasive, the bond that holds it, and the shape that fits your machine. Getting the first two right is what separates a clean grind from a scrapped part.
1. CBN is the correct abrasive for steel
Cubic boron nitride stays hard at grinding temperatures up to ~1400°C and does not react with iron-group metals. Diamond — physically harder — does react with iron at the heat of grinding and converts to graphite, so it disappears on steel. That single fact is why the rule is simple: steel → CBN, everything else hard → diamond.
2. Resin bond cuts cool and finishes smooth
The phenolic resin matrix is slightly flexible. It absorbs vibration, cushions the part, and releases dull grains to expose fresh CBN (self-sharpening). That gives the lowest cutting temperature of the three bond types and the smoothest surface — which is why resin is the default for tool sharpening and finishing. Fiberglass mesh reinforcement keeps the wheel safe at speed.
3. The wheel does the work, not the operator
Because CBN stays sharp and the bond holds form, a single wheel handles rough stock removal through polishing by changing only the grit. You stop fighting heat, loading and constant re-dressing.
Full Specifications
| Product | Resin Bonded CBN Grinding Wheel |
|---|---|
| Abrasive | Cubic Boron Nitride (CBN) — monocrystalline & polycrystalline |
| Bond type | High-temperature phenolic resin, fiberglass-mesh reinforced |
| Hardness grade | Soft (G–H) to Medium-Hard (K–N) |
| Grit / mesh | 46#, 60#, 80#, 100#, 120#, 150#, 180#, 200#, 240#, 280#, 320#, 400#, 500#, 600#, 800#, 1000#, 1200# (custom to 3000#) |
| Grit class | Coarse 46–120 / Medium 120–240 / Fine 280–600 / Polishing 800–3000 |
| Concentration | 75%, 100%, 125%, 150% (standard 100% / 125%) |
| Shapes | 1A1 (straight), 6A2 (cylindrical cup), 11A2 (flaring cup), 12A2, 12V9 (insert), 1A1R, custom |
| Outer diameter (D) | 100, 125, 150, 175, 200, 250, 300 mm (custom to 500/600) |
| Bore (H) | 20, 25.4, 31.75, 50.8, 76.2, 127 mm |
| Thickness (T) | 3, 5, 6, 8, 10, 12, 15, 20, 25 mm |
| Rim width (cup) | 5–25 mm |
| Max operating speed | 35, 40, 50, 60 m/s (up to 125 m/s reinforced) |
| Max RPM (Ø200 @ 60 m/s) | ≈ 5,730 rpm (use marked rating) |
| Surface finish | Ra ≤ 0.2 μm |
| Dimensional tolerance | ±1–5 μm |
| Self-sharpening | Yes — resin wears to expose fresh CBN |
| Thermal stability | Maintains hardness to ~1400°C |
| Coolant | Water-soluble emulsion or light oil (recommended) |
| Best for | HSS, tool steel, die steel (H13 / Cr12MoV), bearing steel (52100), hardened alloy (4140 / 4340), hardened stainless, Ti & Ni superalloys |
| Not suitable for | Tungsten carbide, ceramics, glass, stone, soft non-ferrous (use a diamond wheel) |
| Wheel life vs Al₂O₃ | 30–100× longer |
| Certification | ISO 9001 |
| Color | Brown / black resin body |
| Packaging | Individual box + foam, export carton |
| MOQ | 50 pcs (standard sizes) |
| Lead time | 5–10 days stock; 15–30 days custom |
| Origin | Zhejiang, China |
| Brand | GUSHI |
CBN Wheel vs Diamond Wheel — Choose by Workpiece
This is the one decision that matters most, and it is based purely on the material you are grinding, not on price or brand.
| Dimension | CBN Wheel (this product) | Diamond Wheel |
|---|---|---|
| Hardened steel, HSS, tool/die steel | Correct choice | Wrong — reacts with iron |
| Tungsten carbide, ceramics, glass, stone | Wrong — too slow | Correct choice |
| Chemical affinity with iron | None | Reacts → graphitization at heat |
| Thermal stability | ~1400°C | Lower |
| Surface finish | Ra ≤ 0.2 μm | Ra ≤ 0.2 μm |
| Coolant | Required (ferrous) | Required (most jobs) |
| Typical use | Tool sharpening, steel finishing | Carbide, ceramic, glass |
| Per-part cost on steel | Low (long life) | Very high / fails |
Resin vs Vitrified vs Metal Bond (for CBN)
| Dimension | Resin (this) | Vitrified | Metal |
|---|---|---|---|
| Shock absorption / cool cut | Best | Low | Medium |
| Surface finish | Smoothest | Good | Good |
| Form holding | Medium | Best | Best |
| Wheel life | Medium | Lower | Longest |
| Max speed | 35–60 m/s | Medium | Highest |
| Dressing frequency | Lowest (self-sharpens) | Medium | High |
| Cost | Lowest | Medium | Higher |
| Best for | Tool sharpening, finishing | Form grinding | Heavy stock removal |
Selection Guide
Pick grit by the operation
| Operation | Recommended grit |
|---|---|
| Rough OD / stock removal | #80 – #120 |
| General-purpose grinding | #140 – #200 |
| Fine finishing | #240 – #320 |
| Super-finishing / polishing | #400 and finer |
Pick the bond & concentration by material
- Soft or gummy steel → softer grade (G–H), 75% concentration, more open structure, runs cooler.
- Hardened steel / HSS / die steel → medium grade (K–M), 100–125% concentration — the safe default.
- Long production runs on abrasive steel → 125–150% concentration for longer life between dressings.
- Form-critical profiles → consider vitrified; for finish and forgiveness stay with resin.
How to Use — Safe Grinding Steps
- Mount & ring-test. Confirm the bore matches the spindle, fit the correct bushing and blotters, and ring-test (a clear tone, no cracks) before mounting.
- Dress lightly. True the wheel with a single-point diamond dresser. Resin bond needs only light dressing.
- Set speed. Never exceed the marked max RPM for the wheel diameter.
- Apply coolant. Flood with water-soluble emulsion or light oil — never run dry on steel.
- Grind. Take roughing passes at #80–120, finishing at #240+, keeping depth of cut shallow to avoid heat.
- Re-dress when cutting slows. On resin CBN this is often only every 50–200 parts.
Applications
- HSS tool sharpening — turning tools, milling cutters, drills, reamers (edge Ra ≤ 0.2 μm).
- Die steel cavity finishing — H13, Cr12MoV contour and profile grinding.
- Bearing steel (52100) and gear steel — precision dimensions without burn or cracks.
- Punch grinder / punch former — OD, step, radius and taper grinding.
- Hydraulic valve spools and precision bearing rollers — micron tolerances.
- Hardened stainless, titanium and nickel superalloys — finishing only.
Related superabrasive tools: Diamond Sanding Sheets, Concrete Floor Polishing Pads, Abrasive Sanding Discs.
OEM & Wholesale
GUSHI supplies CBN wheels to toolroom distributors and grinding houses worldwide. We support OEM/ODM and private label, custom shapes (1A1, 6A2, 11A2, 12V9), custom grits to 3000#, and custom bore/bushing to fit your spindle. Samples are available for testing; the sample fee is returned against your first official order.
Frequently Asked Questions
CBN or diamond wheel for my steel part?
Ferrous workpiece (hardened steel, HSS, die steel, cast iron, superalloys) → CBN. Non-ferrous hard-brittle (carbide, ceramic, glass, stone) → diamond. The decision is the material, not the brand.
Why not a cheaper aluminum oxide wheel?
On HRC 58+ steel a CBN wheel lasts 30–100× longer, holds form and stops edge burning. Oxide dulls fast, loads heat and needs constant dressing — slower and more scrap per part.
Can it grind tungsten carbide?
No — use a diamond wheel for carbide/ceramic/glass. CBN removes carbide far too slowly and wears itself out.
Resin, vitrified or metal bond?
Resin (this product) is the all-round choice: cool, shock-absorbing, smoothest finish — best for sharpening and finishing. Vitrified holds form; metal lasts longest for heavy removal.
Do I need coolant?
Yes — always use coolant on ferrous grinding. Resin runs cooler but dry running on steel burns the edge and voids the life expectancy.
What does concentration mean?
It is the volume of CBN in the bond; 100% is standard. 75% is cooler for soft steel; 125–150% lasts longer on hard, abrasive steel and long runs. Default 100–125%.
Speed and safety limits?
Standard 35–60 m/s, reinforced to 125 m/s. RPM ≈ 19100 × speed ÷ diameter. Ring-test, correct bushing/blotters, never exceed marked max RPM, guard the wheel.
MOQ, lead time, OEM, samples?
MOQ 50 pcs standard; 5–10 days stock, 15–30 days custom. OEM/ODM welcome; samples available with fee returned on first order.