Product Overview
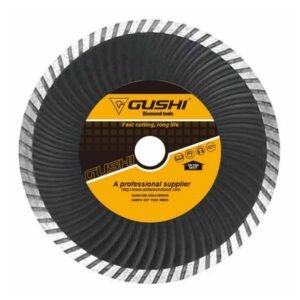
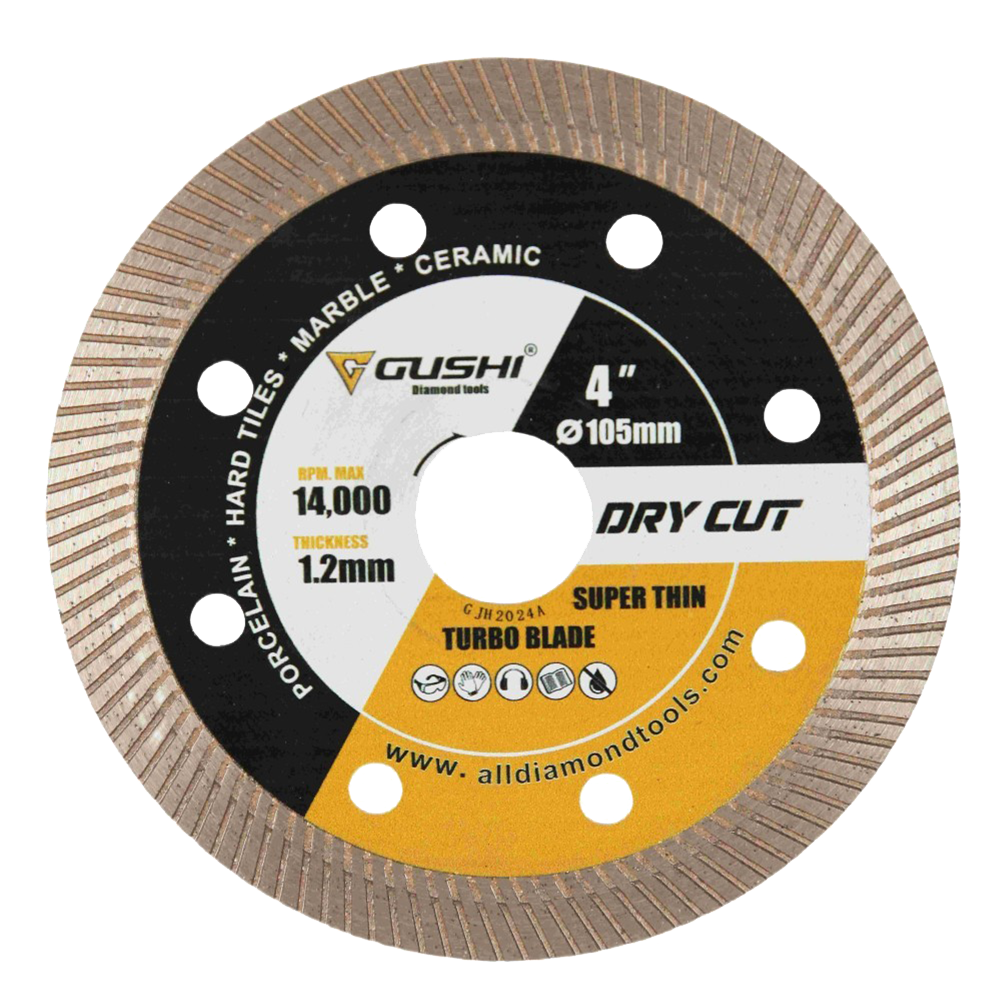
The GUSHI Roycel Super Thin Turbo Diamond Blade is a hot-pressed turbo-rim diamond blade with an ultra-thin 1.0–2.0 mm kerf that delivers chip-free, fast cuts on ceramic, porcelain, granite, marble and stone with minimal dust and material waste. Manufactured by Huzhou Gu’s Imp. & Exp. Co., Ltd. — a diamond tool specialist founded in 2004 and ISO 9001, CE, EN13236 and RoHS certified — the blade pairs a continuous turbo rim (smooth like a continuous rim, fast like a segmented blade) with a strong steel core for both wet and dry use on angle grinders and tile saws. With a production capacity of 100,000 diamond-tool sets per month, GUSHI exports to 20+ countries including the USA, Germany, UK, Australia and Brazil.
The super-thin turbo blade occupies the precision tier of the diamond blade market, where cut quality on brittle, high-value materials matters more than raw demolition speed. Tilers, stone fabricators and renovation contractors choose it for indoor porcelain and ceramic work where chipping ruins expensive slab and dust control is mandatory. The thin kerf also makes it ideal for plunge and curved cuts that a thick segmented blade cannot perform cleanly.
GUSHI is one of only 23 Chinese manufacturers that won the anti-dumping case for diamond blades exported to the USA, holding a 6.2% tariff rate. That compliance heritage, plus in-house hot-pressing and per-lot destructive rim inspection, makes the turbo blade a dependable specification for distributors and OEM partners serving regulated and quality-sensitive markets.
Full Specifications
| Parameter | Specification |
|---|---|
| Product Name | GUSHI Roycel Super Thin Turbo Diamond Blade |
| Model Number | GSDB-TB Series |
| Blade Type | Super thin turbo-rim diamond blade |
| Diameter Range | 105 – 350 mm (4″ – 14″) |
| Arbor / Bore | 20 / 22.23 / 25.4 mm |
| Kerf (Segment) Thickness | 1.0 – 2.0 mm (super thin) |
| Segment Height | 7 / 8 / 10 mm |
| Rim Type | Turbo (serrated continuous rim) |
| Diamond Matrix | Hot-pressed synthetic diamond |
| Bond | Soft–medium, tile / stone optimized |
| Core | Reinforced steel body |
| Max RPM | 5,500 – 15,000 (by diameter) |
| Peripheral Speed | Up to 80 m/s |
| Cutting Mode | Wet and dry |
| Applications | Ceramic, porcelain, granite floor tile, marble, stone, concrete, brick |
| Machines | Angle grinder, tile saw, table saw |
| Certifications | ISO 9001, CE, EN13236, RoHS, SGS |
| Safety Standard | EN13236 (diamond tool safety) |
| Segment Process | Hot-pressed |
| Packaging | Skin card / blister / white box |
| HS Code | 8202.39 |
| MOQ | 500 pieces |
| Lead Time | 25 – 30 days |
| Port of Loading | Shanghai / Ningbo, China |
How the Super Thin Turbo Blade Works
Turbo Rim Geometry
The turbo rim is a continuous diamond rim with regular serrations (turbo teeth) cut into its edge. The continuous portion keeps the cut smooth and chip-free like a continuous-rim blade, while the serrations break the rim into small cooling vents that clear slurry and release heat like a segmented blade. This hybrid geometry lets the blade cut fast on hard tile without the chatter and edge damage a fully segmented blade can cause.
Hot-Pressed Diamond Matrix
The diamond segments are formed by hot-pressing synthetic diamond grit into a metal bond under heat and pressure. Hot-pressing produces a denser, stronger segment than cold pressing, holding the diamond particles firmly so they wear evenly and stay sharp longer. A soft–medium bond is selected for hard, brittle tile so the matrix releases spent diamond at the right rate and maintains cutting speed.
Super-Thin Kerf Physics
The 1.0–2.0 mm kerf removes far less material per pass than a 3 mm segmented blade. Less material to cut means less drag on the motor, less friction heat and a narrower cut line — which directly reduces dust, vibration and the chance of chipping on porcelain and ceramic. The turbo vents compensate for the thin profile by keeping the rim cool during fast, continuous cuts.
Key Features Explained
Ultra-Thin 1.0–2.0 mm Kerf
The thin kerf removes minimal material, producing up to 40% less dust and virtually no chipping on brittle surfaces. On expensive porcelain and quartz, that means a clean edge straight off the saw with little or no grinding required.
Turbo Rim — Smooth and Fast
The serrated continuous rim combines continuous-rim smoothness with segmented-blade speed. The result is fast, chip-free cutting and the ability to make plunge and curved cuts that a thick segmented blade cannot do cleanly.
Hot-Pressed Bond Longevity
Hot-pressed segments are denser and more wear-resistant than cold-pressed equivalents, holding diamond firmly for a stable, long service life. With water cooling, a 10 mm segment blade commonly reaches 800–1,500 linear meters on ceramic and porcelain.
Low Vibration and Dust
The balanced thin core and turbo rim generate less vibration and dust than thick segmented blades, improving operator comfort and making indoor, dust-controlled jobs safer and cleaner.
Universal Arbor Fit
With 20, 22.23 and 25.4 mm arbor options across the size range, the blade fits most standard angle grinders, handheld tile saws and table saws without adapters — simplifying procurement for distributors.
EN13236 Compliance
Every blade is manufactured and tested to the EN13236 diamond-tool safety standard, the European benchmark for rotating diamond tools. QC includes destructive rim and core cross-section inspection, with SGS inspection available on request.
Selection / Diameter Guide
Match diameter and arbor to your machine and the material thickness. Smaller sizes with 20/22.23 mm arbors fit angle grinders and handheld tile saws; larger 300–350 mm blades with 25.4 mm arbors suit table and bridge saws.
| Diameter | Arbor (mm) | Machine | Best For |
|---|---|---|---|
| 105 mm (4″) | 20 | 4″ angle grinder | Ceramic wall tile, indoor trim |
| 115 mm (4.5″) | 22.23 | Angle grinder | Porcelain, floor tile |
| 125 mm (5″) | 22.23 | Angle grinder, tile saw | Granite floor tile, marble |
| 150 mm (6″) | 22.23 | Tile saw, grinder | Marble, natural stone |
| 180 mm (7″) | 22.23 | Tile saw, grinder | Granite slab edge, stone |
| 200 mm (8″) | 22.23 | Tile / table saw | Thick porcelain, pavers |
| 230 mm (9″) | 22.23 | Tile / table saw | Concrete, brick, stone |
| 300 mm (12″) | 25.4 | Table saw | Granite, marble slabs |
| 350 mm (14″) | 25.4 | Table / bridge saw | Stone fabrication |
Applications & Suitable Materials
Where the Super Thin Turbo Blade Excels
| Application | Why the Turbo Blade Wins |
|---|---|
| Porcelain & ceramic tiling | Chip-free edges, minimal dust indoors |
| Granite / marble floor tile | Clean cut face, low vibration |
| Indoor renovation | Low dust, quiet, plunge cuts |
| Curved & plunge cuts | Thin kerf follows tight profiles |
| Stone fabrication trim | Smooth edge, little rework |
| Light concrete & brick | Acceptable with wet cooling |
Suitable Materials
| Material | Bond Recommendation | Cutting Mode |
|---|---|---|
| Porcelain, ceramic | Soft bond, sharp grit | Wet / dry |
| Granite floor tile | Soft–medium bond | Wet preferred |
| Marble, limestone | Soft bond | Wet / dry |
| Engineered stone | Soft–medium bond | Wet |
| Light concrete, brick | Medium bond | Wet / dry |
| Natural stone | Medium bond | Wet |
Super Thin Turbo vs. Standard Segmented Blade
Both are diamond blades, but they are built for different jobs. The table compares the GUSHI super thin turbo blade with a conventional thick segmented blade at a similar diameter.
| Dimension | Super Thin Turbo (GUSHI) | Standard Segmented Blade |
|---|---|---|
| Kerf width | 1.0–2.0 mm (thin) | 2.4–3.6 mm (thick) |
| Cutting speed (tile) | Faster, less drag | Slower on thin tile |
| Chipping on tile | Minimal | Higher risk |
| Dust generation | Lower (up to 40% less) | Higher |
| Material waste | Less (thin kerf) | More |
| Edge finish | Smooth, chip-free | Rougher |
| Cooling | Turbo vents aid cooling | More gullets (best cooling) |
| Curved / plunge cuts | Excellent | Poor |
| Blade lifespan | Thinner (shorter total) | Longer (thick segment) |
| Best for | Tile, porcelain, indoor | Concrete, masonry, asphalt |
| Initial cost | Higher per blade | Lower |
Bottom line: Choose the super thin turbo blade for tile, porcelain, granite tile and any indoor, dust-sensitive or curved cut. Choose a standard segmented blade for heavy concrete, reinforced concrete, asphalt and demolition where raw cutting depth and lifespan outweigh edge finish.
How to Use: Step-by-Step Guide
- Confirm the blade arbor (20, 22.23 or 25.4 mm) matches your angle grinder, tile saw or table saw spindle.
- Inspect the rim and core for cracks, missing diamond or loose segments; never use a damaged blade.
- Mount the blade with the correct flange and tighten to spec; check the rotation arrow matches spin direction.
- Verify your machine’s maximum RPM exceeds the blade’s rated RPM for its diameter (105 mm up to 15,000 RPM).
- Mark the cut line on the tile; for plunge cuts, start from the edge rather than forcing into the face.
- For wet cutting, connect water to the cut zone before starting — it suppresses dust and protects the bond.
- Begin with light feed pressure; let the turbo rim do the cutting instead of pushing the blade.
- Keep a steady, even feed; the thin kerf needs little force, so avoid leaning on the grinder.
- Use the turbo rim’s agility for curved and notch cuts that a thick blade cannot follow.
- If dry cutting, pause every 30–60 seconds to let the rim cool; never force a hot blade.
- After cutting, wipe the rim clean of slurry and diamond paste to keep it cutting freely.
- Store the blade flat in its protective sleeve — never lean it where the thin core can warp.
For more guidance, see our related guides on Diamond Core Drill Bits, Diamond Polishing Pads, and Diamond Cup Grinding Wheels.
Preguntas frecuentes
What is a super thin turbo diamond blade and how is it different from a standard blade?
A super thin turbo blade has a serrated continuous (turbo) rim and an ultra-thin 1.0–2.0 mm kerf. The turbo rim merges the chip-free smoothness of a continuous rim with the fast cutting and cooling of a segmented blade, while the thin kerf reduces drag, dust and material waste. A standard segmented blade has a thicker 2.4–3.6 mm kerf and deeper gullets built for aggressive concrete and masonry work, not fine tile cutting.
What materials can the super thin turbo diamond blade cut?
It cuts ceramic tiles, porcelain, granite floor tiles, marble, engineered stone, and natural stone, plus light concrete, brick and masonry. Soft-to-medium bond formulas are tuned for hard, brittle tile materials to give chip-free edges. For heavy reinforced concrete, asphalt or green concrete, a thicker segmented blade is the better choice.
Can the turbo blade be used wet and dry?
Yes. The blade is rated for both wet and dry cutting. Wet cutting suppresses dust and cools the rim, which is preferred for indoor tiling and continuous runs. Dry cutting is fine for fast on-site work on angle grinders — use intermittent feed and allow cool-down breaks every 30–60 seconds to protect the hot-pressed bond.
What diameters and arbor sizes are available?
Diameters range from 105 mm (4″) to 350 mm (14″). Small 105–230 mm blades use 20 or 22.23 mm (7/8″) arbors for angle grinders and handheld tile saws; 300–350 mm blades use a 25.4 mm (1″) arbor for table and bridge saws. Segment height options are 7, 8 and 10 mm, with kerf scaled 1.0–2.0 mm by diameter.
Why does the thin kerf matter for tile and porcelain?
A 1.0–2.0 mm kerf removes far less material than a 3 mm segmented blade, so there is less drag, less heat and far less chipping on brittle porcelain and ceramic. That means cleaner edges (often no need to grind), up to 40% less dust, and minimal wasted material on expensive slab. The turbo rim vents keep the cut cool despite the thin profile.
How long does a super thin turbo blade last?
Lifespan depends on material hardness and cooling. On ceramic and porcelain with water cooling, a 10 mm segment blade typically delivers 800–1,500 linear meters of cut. The thin kerf uses less diamond per cut than a thick blade, so per-meter cost stays competitive even though total blade life is shorter than a heavy segmented blade.
What is the OEM minimum order quantity and lead time?
OEM and private-label MOQ is 500 pieces per specification. Standard production lead time is 25–30 days after artwork and sample confirmation. Custom branding (laser marking, silk screen or printed stickers), packaging and bond formulas are available. Samples are supplied at cost price with the buyer paying shipping. Payment via L/C, T/T, Western Union or PayPal. Port of loading: Shanghai or Ningbo.
Is the turbo diamond blade certified for international markets?
Yes. GUSHI super thin turbo blades are manufactured under ISO 9001:2015, carry CE marking and RoHS compliance, and are tested to the EN13236 diamond-tool safety standard that governs European diamond-blade use. Each lot is QC-checked with destructive rim and core inspection, and SGS inspection is available on request.
OEM & Wholesale Information
| Parameter | Specification |
|---|---|
| Minimum Order Quantity | 500 pieces per specification |
| Production Lead Time | 25 – 30 days after sample & artwork confirmation |
| Custom Branding | Laser marking, silk screen, printed stickers |
| Custom Packaging | Skin card, blister, white box |
| Custom Specifications | Diameter, kerf, segment height, bond per RFQ |
| Sample Policy | Available at cost price; buyer pays shipping |
| Payment Terms | L/C, T/T, Western Union, PayPal |
| Port of Loading | Shanghai or Ningbo, China |
| QC Documentation | Destructive rim/core inspection per lot, SGS on request |
| Production Capacity | 100,000 diamond-tool sets / month |
Huzhou Gu’s Imp. & Exp. Co., Ltd. (GUSHI Tools / Roycel) has manufactured and exported diamond tools since 2004, serving 20+ countries across North America, Europe, South America, Australia and Africa. As one of 23 Chinese companies that won the US anti-dumping case for diamond blades (6.2% tariff rate), GUSHI combines compliant export experience with ISO 9001, CE, EN13236 and RoHS certified production. Many distributor partners have collaborated with GUSHI for over 10 years.